Extreme Environmental Testing Chambers for 5G & Telecom
5G networks demand significantly higher frequencies and massive MIMO (Multiple Input, Multiple Output) architectures. This exponential increase in data processing creates unprecedented environmental and thermal challenges for telecom equipment based on rooftops, cell towers, and coastal regions
The Fabrication Challenge
5G networks demand significantly higher frequencies and massive MIMO (Multiple Input, Multiple Output) architectures. This exponential increase in data processing creates unprecedented environmental and thermal challenges for telecom equipment based on rooftops, cell towers, and coastal regions
Massive Active Heat Loads (Thermal Throttling)
5G AAUs and Baseband Units (BBUs) consume up to 3x more power than 4G equipment. When deployed in desert climates (ambient temperatures exceeding 50°C) with direct solar radiation, the internal active heat load is immense. If the heat sink design fails to dissipate this energy, the processors thermal throttle, resulting dropping network speeds and eventually causing critical semiconductor failure
Coastal Salt Fog & Galvanic Corrosion
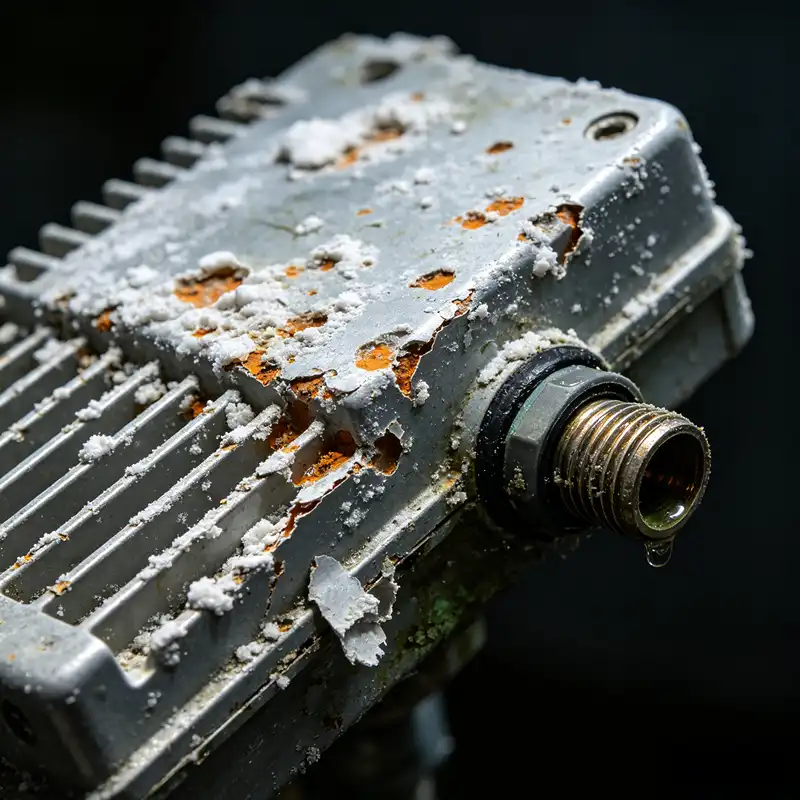
Telecom enclosures are built to last 10-20 years outdoors. In coastal deployments, windblown salt fog relentlessly attacks the aluminum heat sinks, galvanized brackets, and weather-sealed RF connectors. Salt acts as an electrolyte, accelerating galvanic corrosion between dissimilar metals, it destroys the IP65 waterproof seals and allows conductive saline moisture to short-circuit the internal PCBs
Optical Transceiver Thermal Fatigue
The fiber-optic transceivers (SFP, QSFP modules) connecting base stations to the core network are incredibly delicate. As temperatures swing from freezing nights to scorching days, the disparate thermal expansion rates between the silicon photonics, gold wire bonds, and ceramic substrates cause violent shear stress. This eventually snaps the microscopic connections, resulting in catastrophic signal loss (dark fiber)
Why 5G & Telecom need Climatic testing Chambers?
Component Level (Thermal Shocking Photonics)
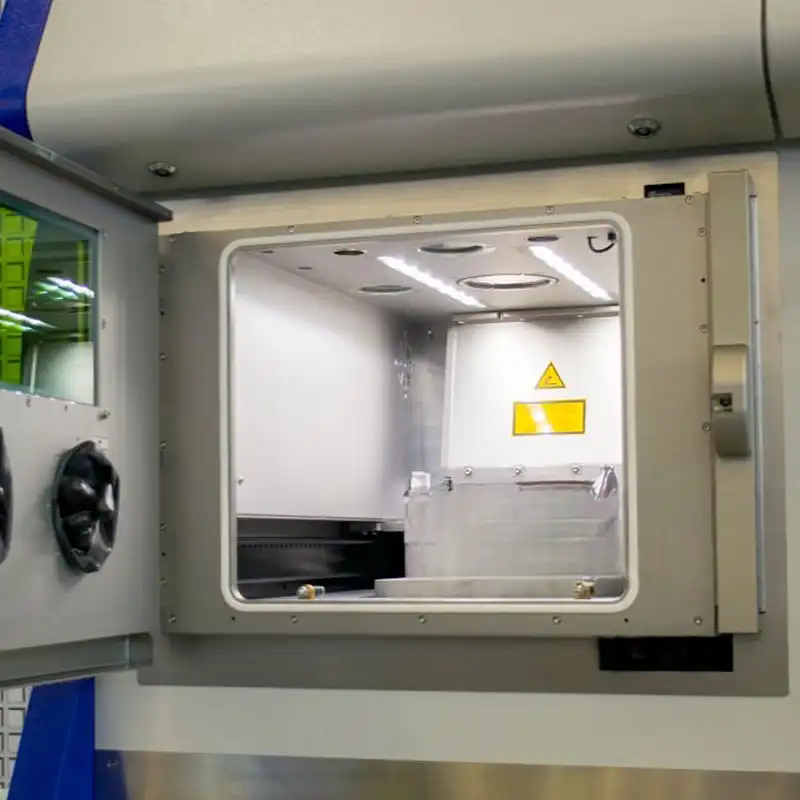
Delicate 100G/400G optical transceivers and high-frequency RF chips are placed into JCT Thermal Shock Chambers. The system violently shifts the components from -40°C to +85°C in under 10 seconds. This aggressively screens out weak wire bonds, defective epoxies, and mismatched thermal expansion rates in the silicon photonics before they are assembled into the RRU
Enclosure Level (Cyclic Salt Spray)
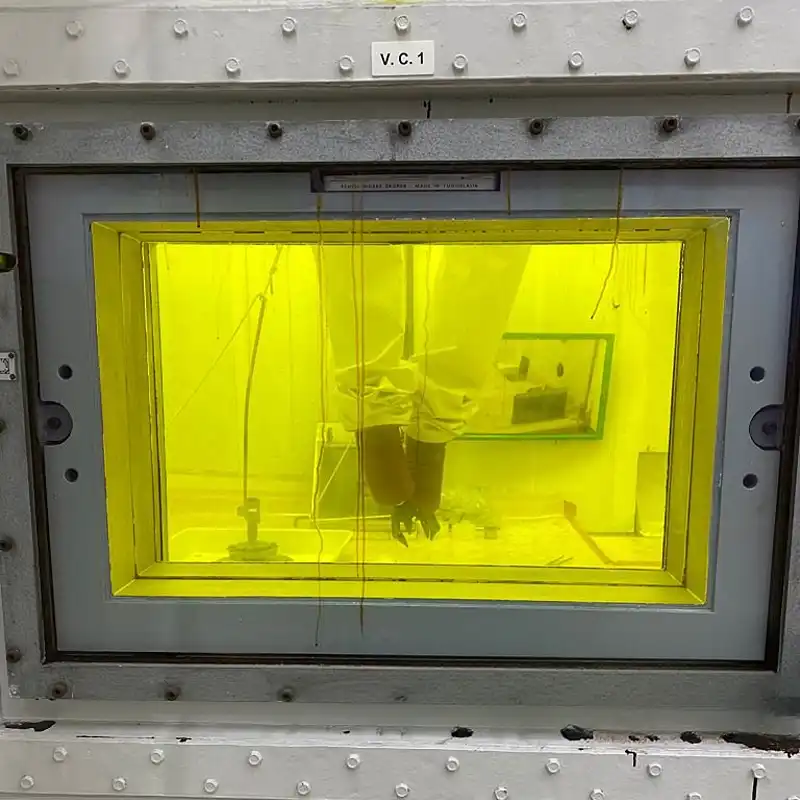
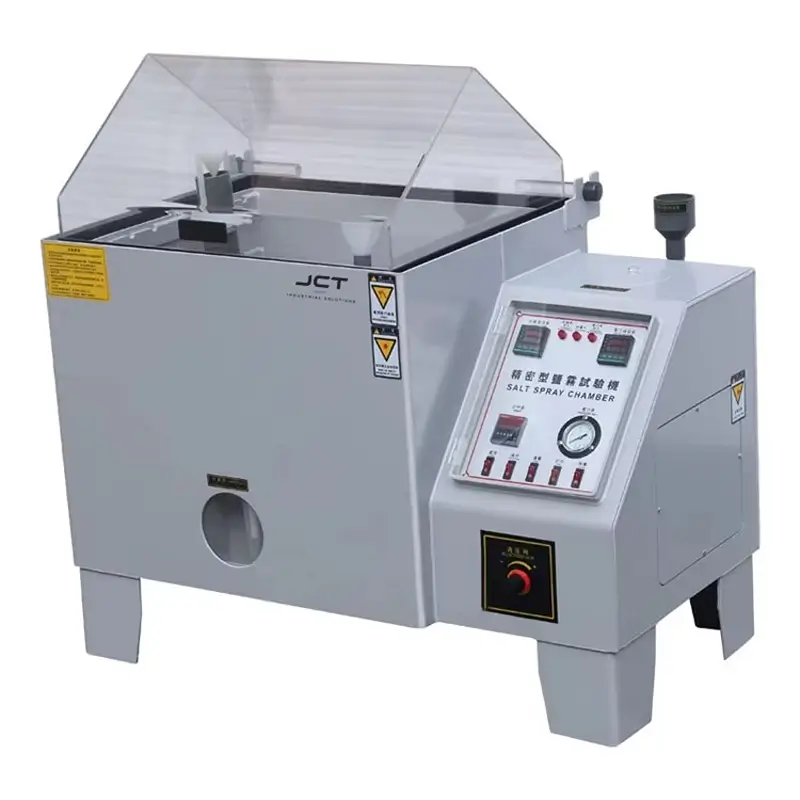
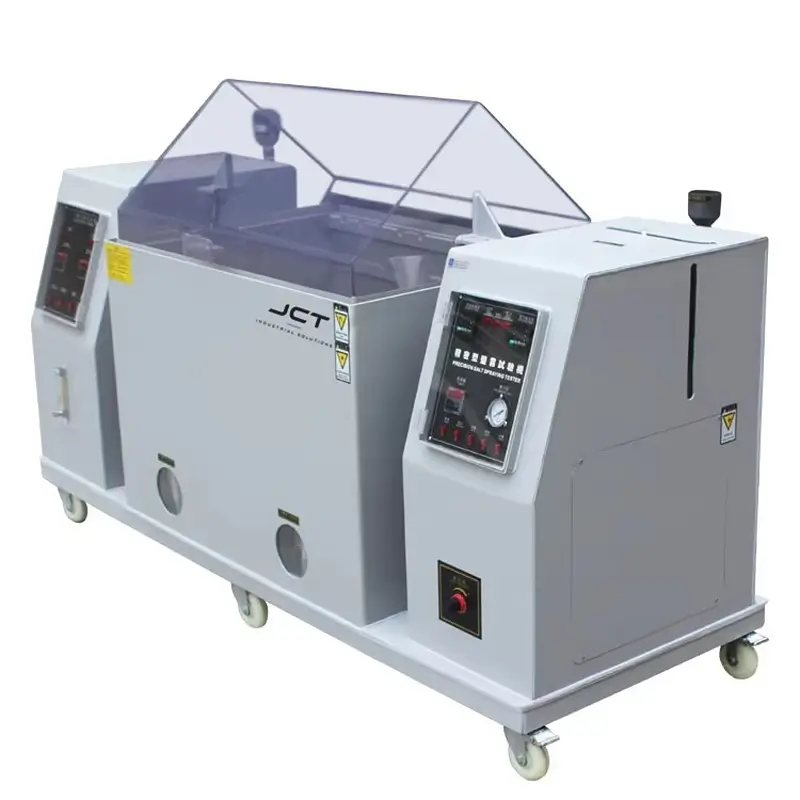
The bare aluminum RRU enclosures, powder-coated brackets, and RF cable connectors are loaded into JCT Salt Spray Chambers. By cycling between highly corrosive saline fog, high humidity, and drying phases, engineers can validate the lifespan of anti-corrosion coatings and the galvanic compatibility of fasteners used for coastal cellular deployments.
for 5G &Telecom Testing We CAN Supply
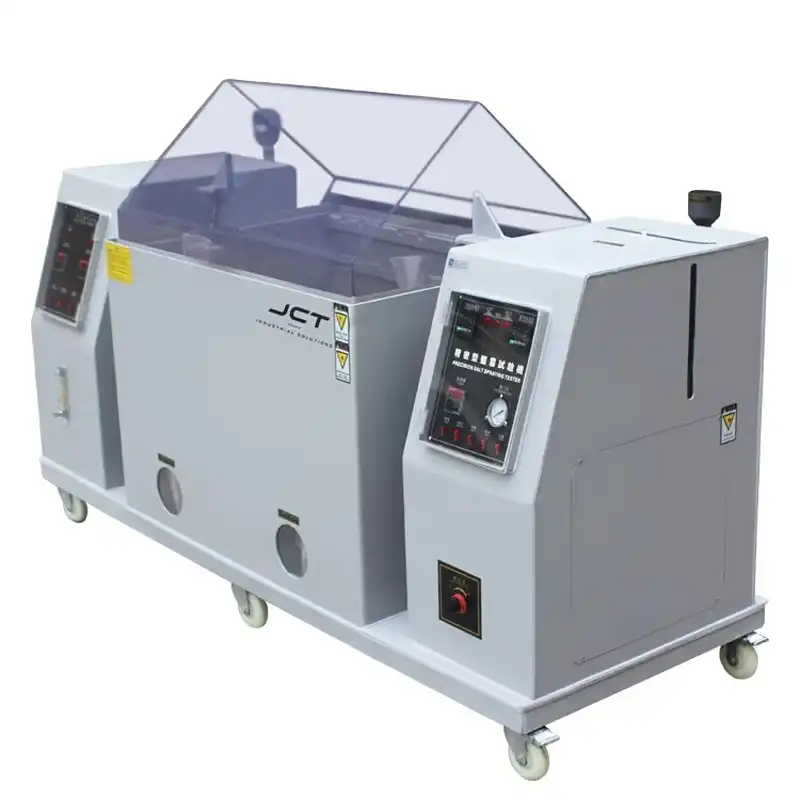
Outdoor RRU enclosures, galvanized mounting brackets, RF antennas, and weather-sealed connectors.
- Goes beyond basic static salt fog. Executes advanced programmable cycles including salt mist, high humidity, drying, and ambient resting to simulate real-world coastal corrosion strictly per IEC 60068-2-52 and Telcordia standards. Constructed from heavy-duty titanium and specialized plastics to resist internal degradation.
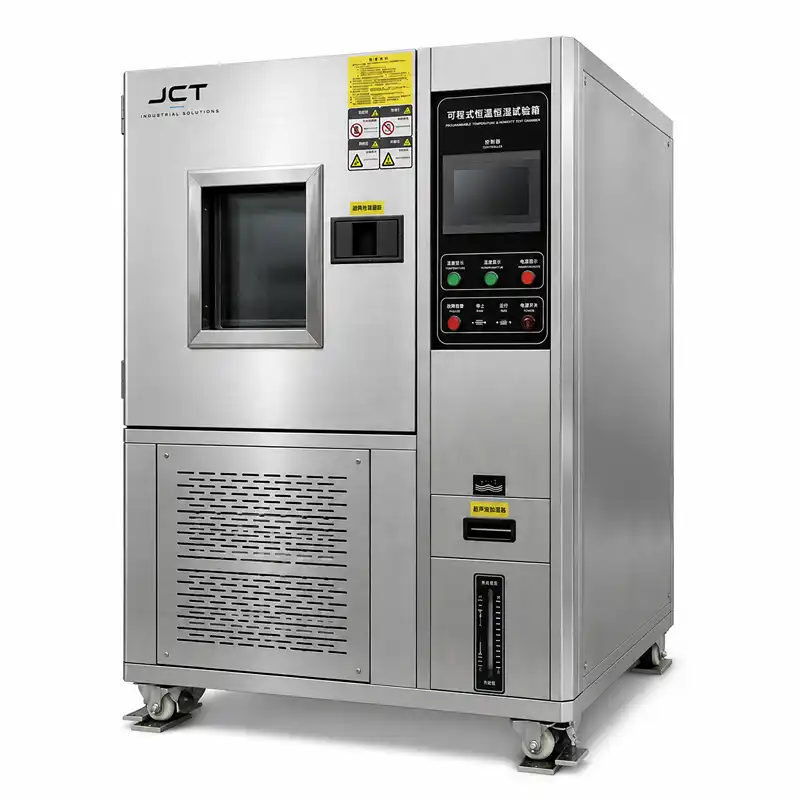
High-speed optical transceivers (SFP/QSFP), RF filters, and high-density telecom PCB solder joint reliability
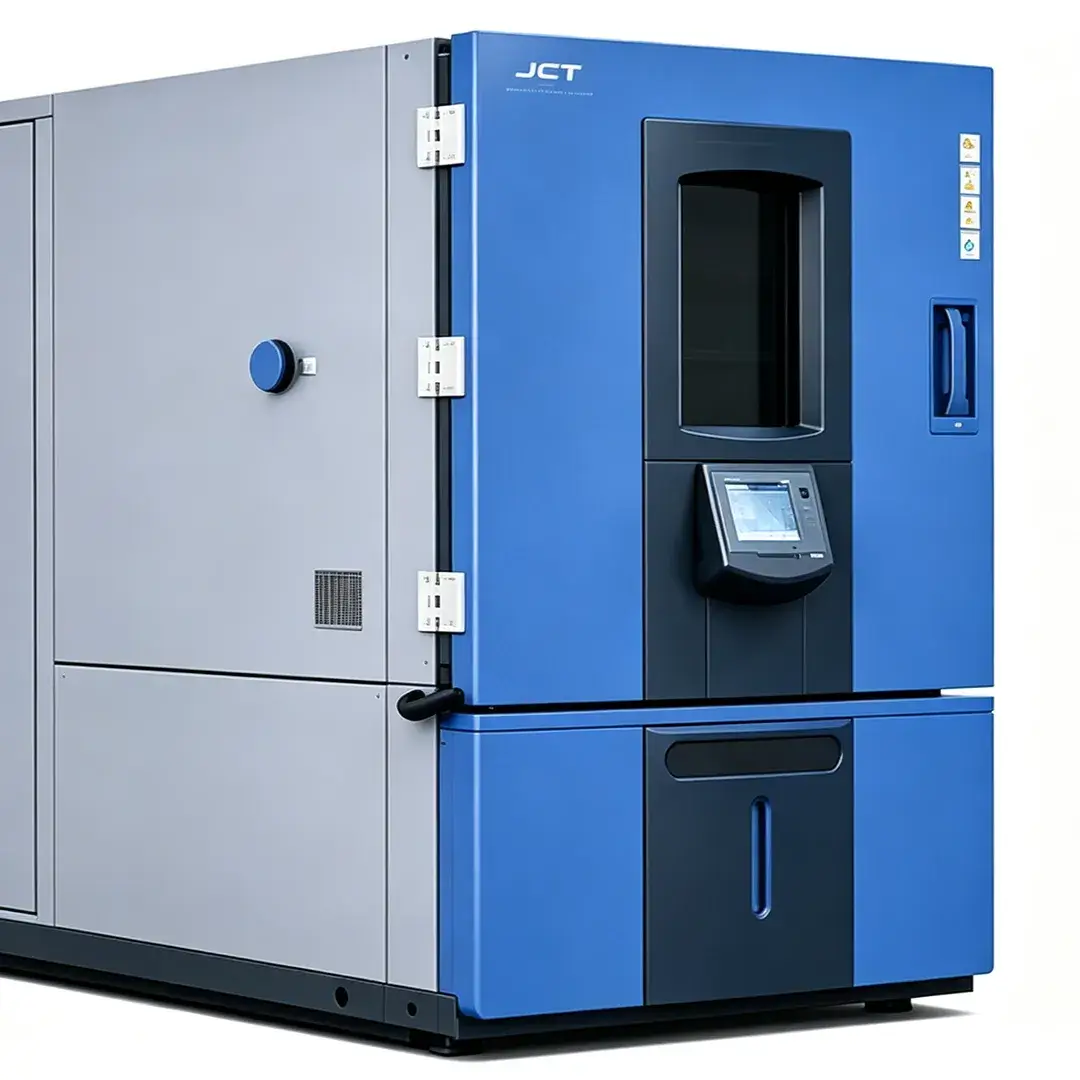
Maximum thermomechanical stress. A pneumatic basket transfers delicate electronic components between extreme hot and cold zones in under 10 seconds. Exposes CTE mismatches and screens out latent manufacturing defects in photonics and microprocessors before they are integrated into expensive core network hardware.
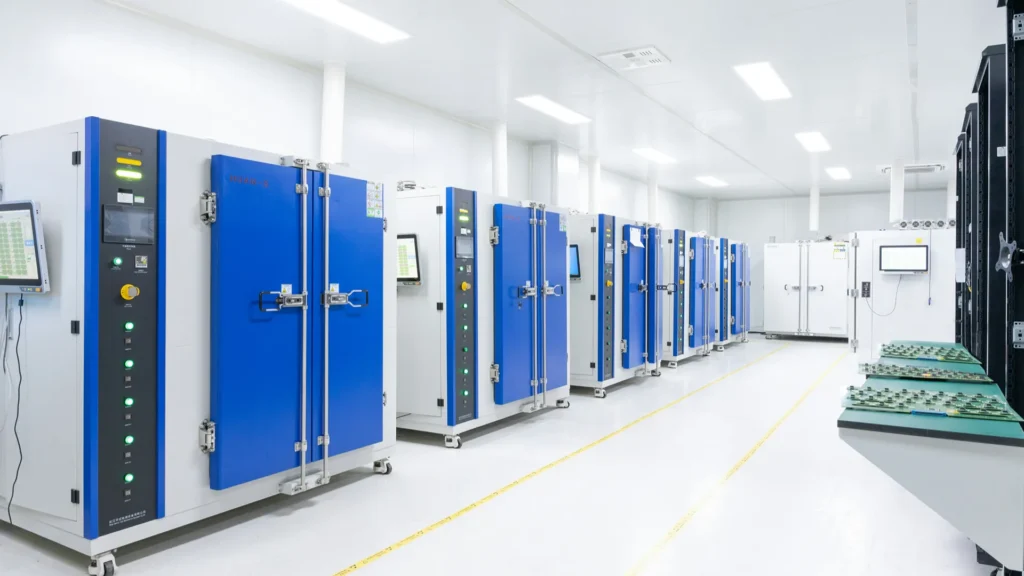
Direct Manufacturer of Environmental Test Chambers
WHO WE ARE?
We build environmental test chambers. We help you test raw materials and finished products under extreme conditions. We find potential quality risks before mass production, protecting your products from costly returns.
With over 10 years of industry experience, we cover a full range of equipment: +180℃ high temperature, -70℃ to +180℃ temperature & humidity, thermal shock, and salt spray corrosion chambers.
We have strong R&D and manufacturing power. We accept custom orders to match your exact test standards.
We hold over 30 patents. We are ISO9001 and CE certified. Our products are exported to 50+ countries, including Europe, North Europe, Australia, Latin America, and Southeast Asia.
We are the direct source factory—no middlemen. Choose JCT, and let us safeguard your product quality.
We hold multiple product patents. We are ISO9001 and CE certified.
Choose JCT. Choose a lifelong partner.
OUR CORE ADVANTAGES
Why Choose Us
With over 10 years of rich industry experience, we are committed to served as a comprehensive technology manufacturer partner worldwide.We understand that your successful product relies on two core pillars: efficient manufacturing and uncompromising quality control.As a result, we offer a dual-core product line: first, laser and FAB solutions that ensure efficient manufacturing; and second, environmental test chambers for testing the performance of your products—all designed to address your specific industry issues and challenges.
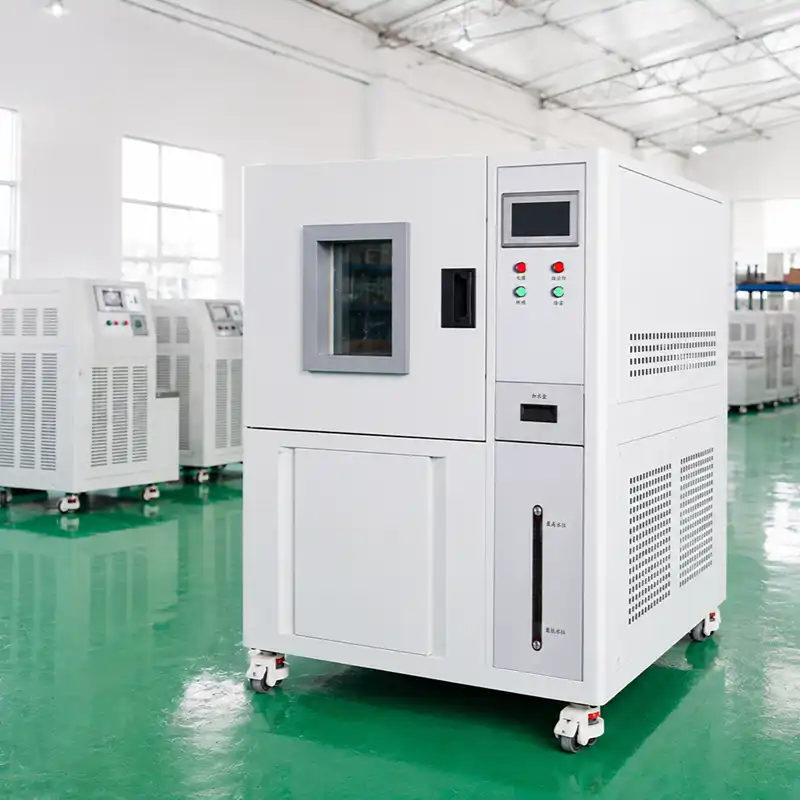
Industry-Specific Customization
Whether you’re in the sheet metal or metalworking industries, or specialize in testing semiconductors and automotive electronics, our equipments all can be customized to meet your specific needs. We don’t just sell standard machines—we provide precise solutions that perfectly match your material and environmental requirements.
High-Efficiency Manufacturing
In the manufacturing process, time is your most valuable treasure. We offer fiber laser welding, cutting, and cleaning,etc solutions . All of them can provide deep penetration, distortion-free welding, precise cutting, and efficient cleaning for sheet metal and various types of metal processing.
Compliance and Quality Control
We ensure that your finished products can pass the most rigorous environmental testing. Our environmental test chambers help you meet strict global standards such as JEDEC, AEC-Q100, and key battery safety certifications, all these can shorten your R&D cycle and eliminating the risk of customer returns .
10+ Years & Global Support
With over a decade of technical expertise and a robust supply chain, we guarantee on-time delivery worldwide. More importantly, our engineering team will provide lifetime technical support, and we are committed to being your stable and reliable partner and friend for life.
PREMIUM COMPONENTS ASSURANCE
Certified to Global Leading Standards
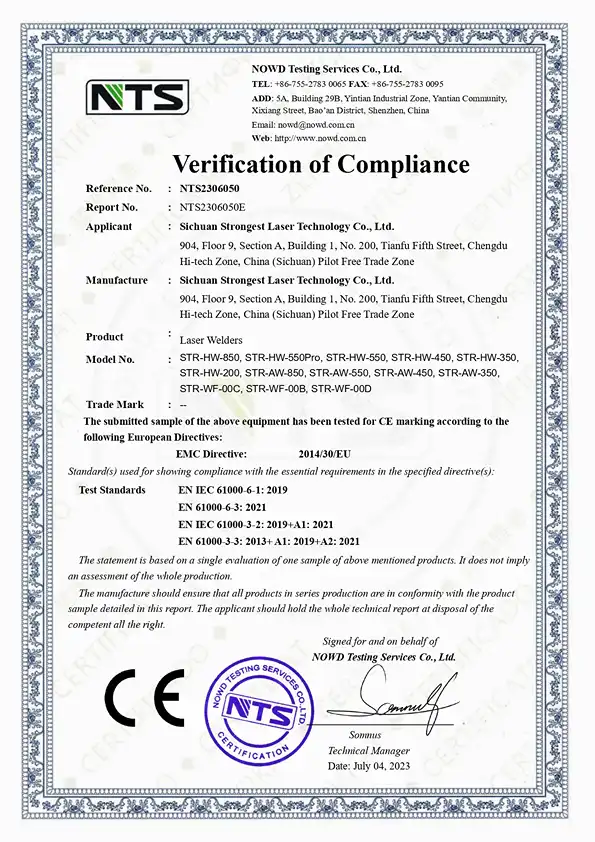
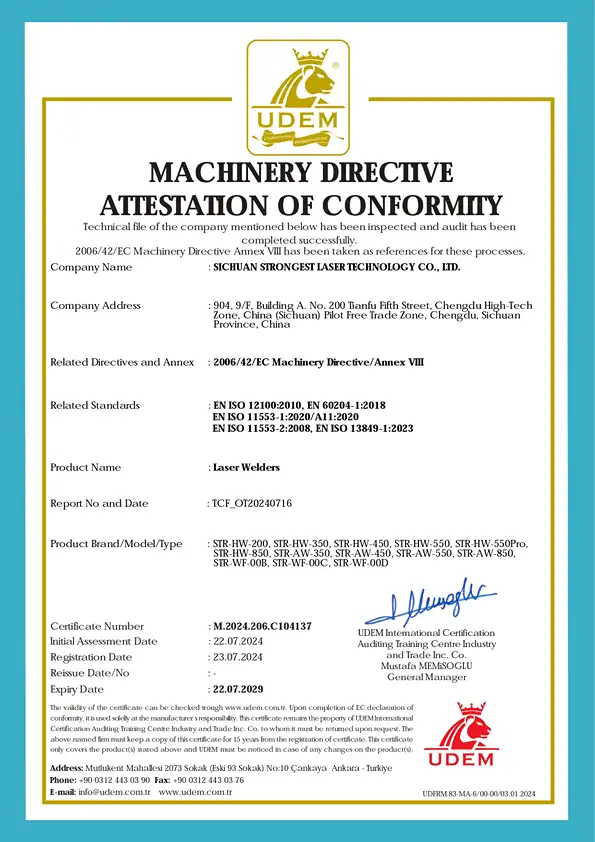
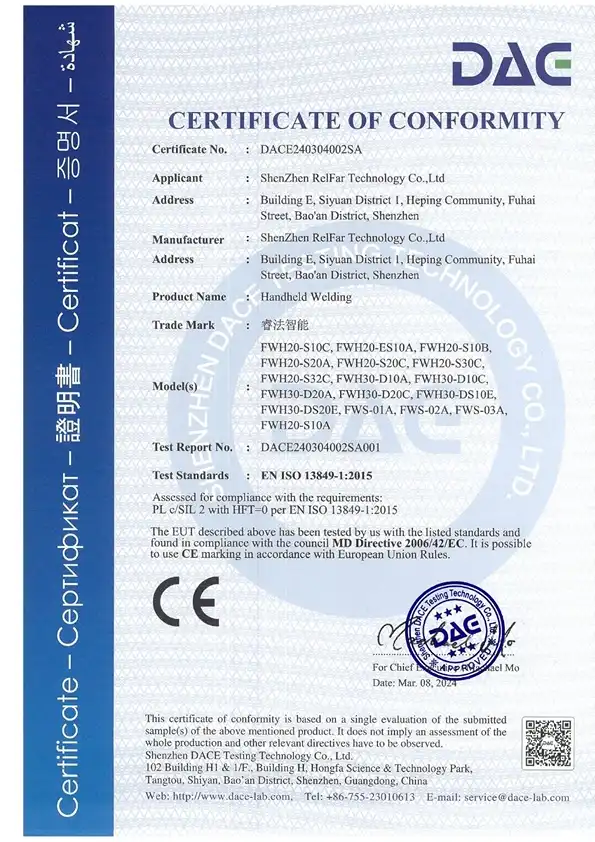
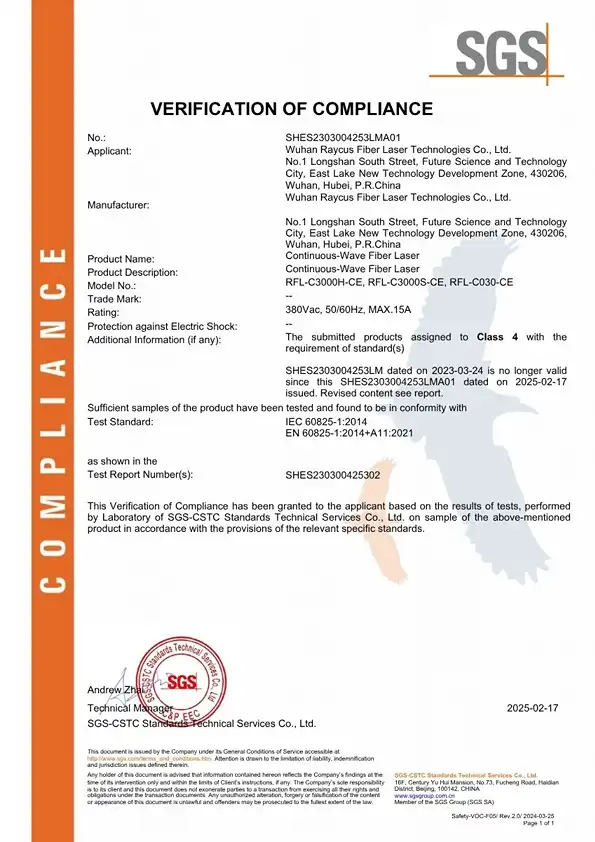
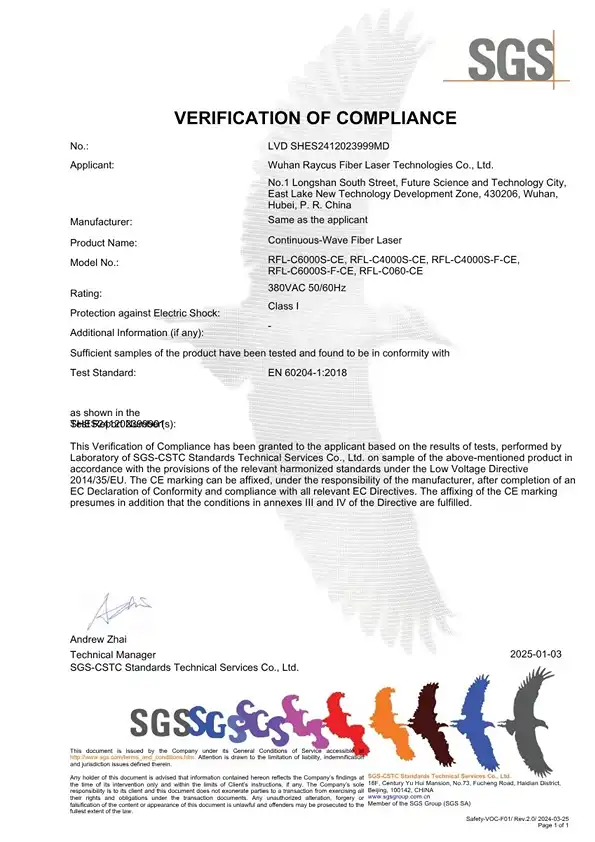
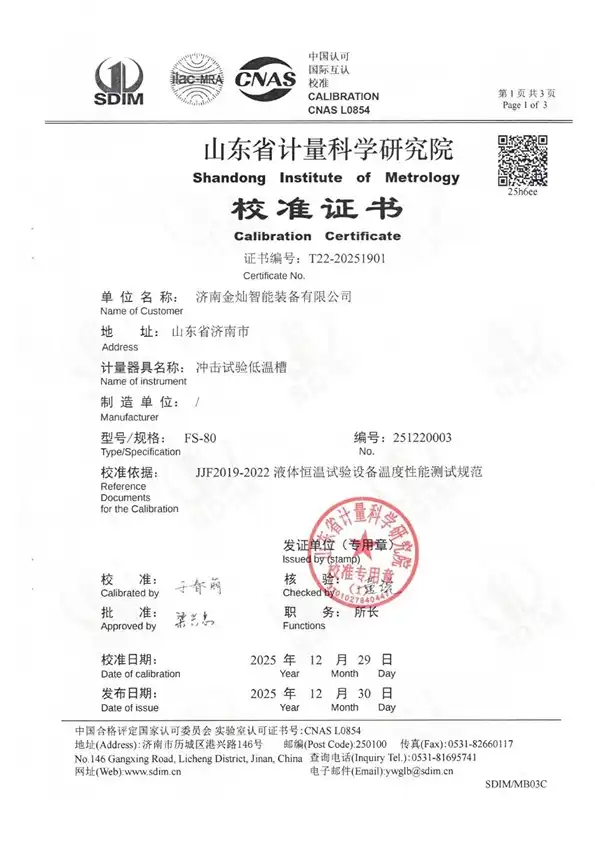
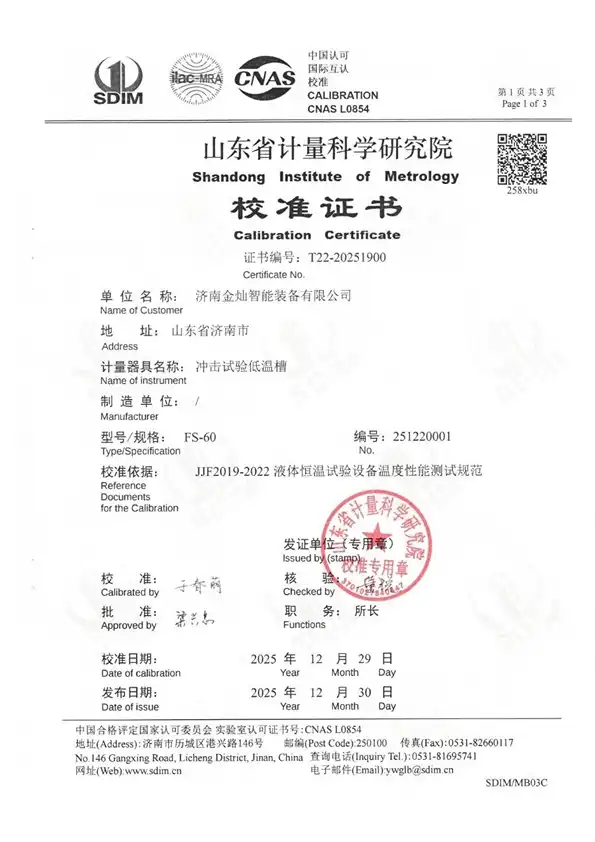
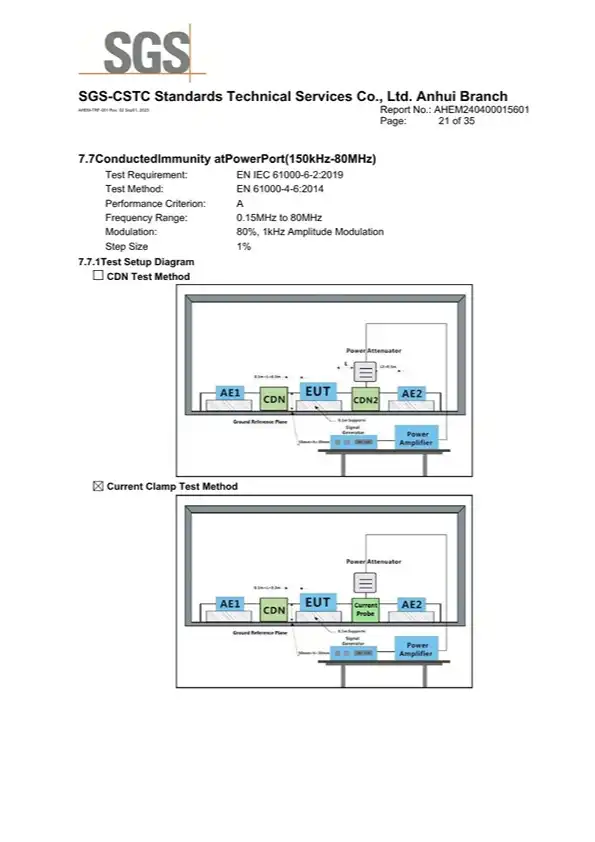
Reliability starts at the core. The key components that power our equipment—from the laser source to even the smallest electronic components—have all been certified to meet the world’s most stringent international standards.
GLOBAL PARTNERSHIPS
Trusted by Industry Leaders Worldwide
We take pride in powering the success of top-tier global manufacturers, research institutions, and industrial leaders. Our advanced laser and testing solutions are trusted worldwide to deliver uncompromising quality and peak performance.
FAQ
Q1: How do we test if our outdoor telecom cabinet will suffer from internal condensation during the winter?
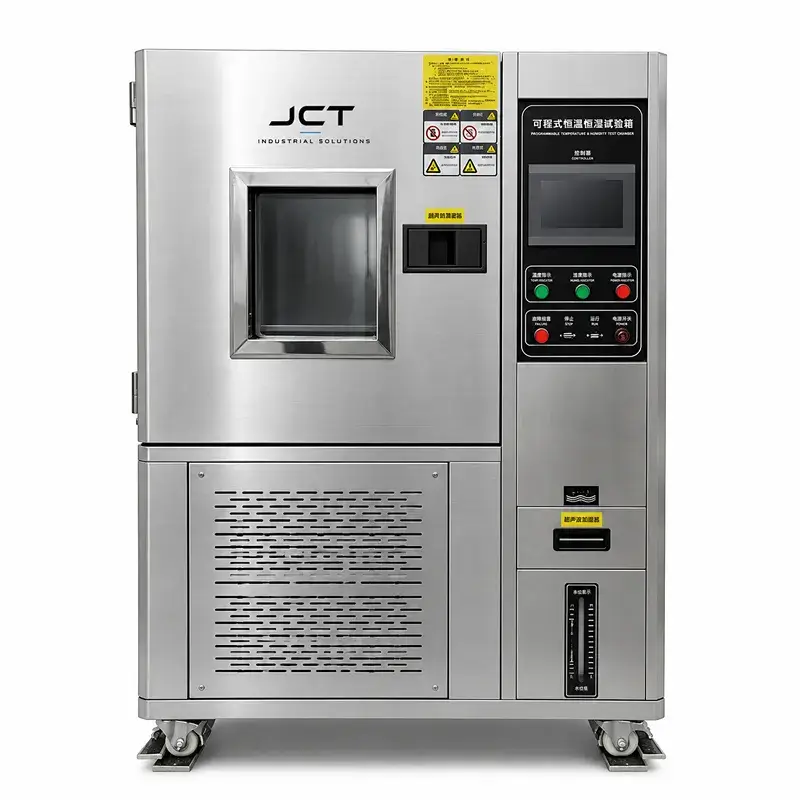
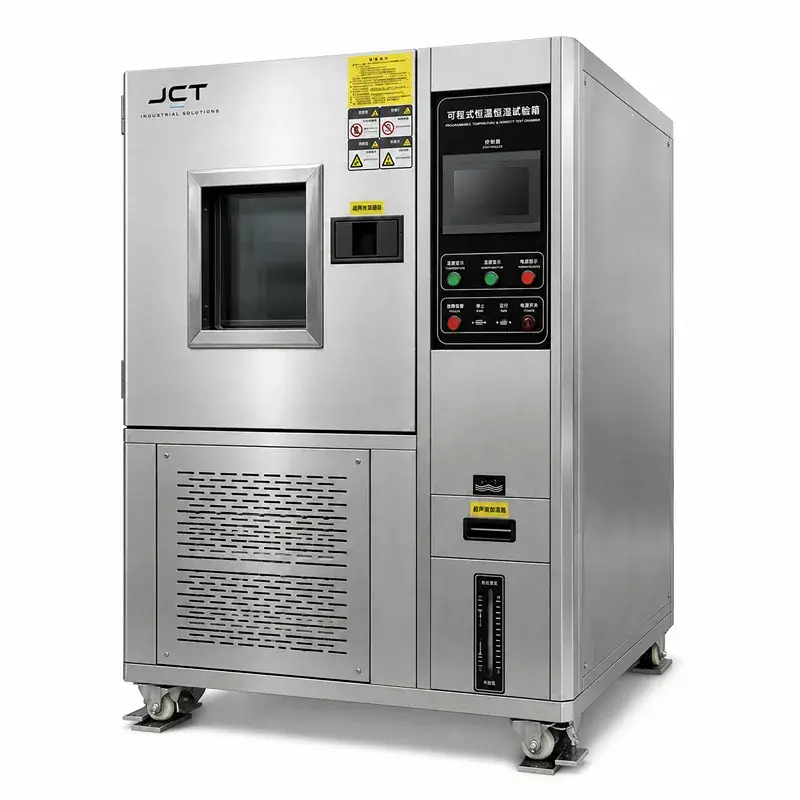
You can utilize a Temperature & Humidity Climatic Chamber. By ramping the external temperature down rapidly while maintaining internal heat (simulating a cold night), you can force dew-point conditions. This validates the effectiveness of your cabinet’s internal heaters, Gore-Tex breather vents, and humidity management systems.
Q2: We need to test an active 5G antenna transmitting data. How do we get the cables inside the chamber?
JCT chambers feature specialized, hermetically sealed access ports. You can route thick RF cables, fiber optics, and heavy DC power lines from your external testing rigs directly into the chamber without compromising the temperature or humidity seal.
Q3: How fast can the Thermal Shock chamber transfer our optical transceivers between temperatures?
Our 2-Zone pneumatic basket systems are designed to transfer your test payload from the extreme hot zone (+150°C) to the extreme cold zone (-65°C) in under 10 seconds. This rapid transfer is strictly required by ETSI and Telcordia standards to induce maximum thermal fatigue on solder joints.
Q4: What maintenance is required for a cyclic salt spray chamber?
Salt spray chambers require diligent maintenance due to their corrosive nature.
You must use high-purity deionized (DI) water and precise NaCl mixtures to prevent nozzle clogging. The internal brine tank must be cleaned regularly, and the atomizing nozzles should be inspected monthly to ensure uniform fog distribution
Q5: What is the ROI for a telecom equipment manufacturer investing in in-house chambers?
The ROI is typically realized within the first major product rollout (3 to 6 months).
Outsourcing live-load telecom testing to third-party labs is incredibly expensive and delays R&D iteration by months. In-house testing allows you to pass carrier audits faster, and entirely avoids the catastrophic brand damage of deploying thousands of base stations that fail during their first winter.
Related Products
Get a Factory-Direct Custom Quote
Do not let massive live heat loads or coastal salt fog destroy your network infrastructure.
Tell our environmental engineering team about your testing requirements (e.g., Telcordia, ETSI), the physical dimensions of your telecom cabinets, and your maximum live thermal heat load. We will recommend the exact JCT testing chamber to secure your carrier contracts, complete with a factory-direct quote within 12 hours.