Airtight Laser Welding & Cleaning for HVAC Ductwork
JCT’s advanced laser processing solutions enable the production of high-pressure HVAC pipes and ducts with excellent airtightness, completely eliminating issues such as leaks at mechanical joints, toxic bituminous sealants and burn-through of thin sheets; the products comply directly with the SMACNA Class 3+ standard.
The Fabrication Challenge
Manufacturing warehouse pallet racks, cantilever shelving, and mezzanine platforms requires joining thick structural carbon steel (typically 2.0mm to 6.0mm+). Relying on high-amperage MIG welding creates severe structural and cosmetic bottlenecks
Incomplete Root Penetration (Catastrophic Risk)
Heavy-duty pallet racks must hold thousands of pounds. Traditional MIG welding often suffers from “cold lap” or lack of root fusion on thick baseplates and uprights. The weld just sits on the surface rather than penetrating deeply, this will creat a hidden weak point that can lead to catastrophic rack collapse under dynamic forklift loads.
The Mill Scale and Rust Barrier
Structural carbon steel arrives from the mill ,they have covered in a hard, dark oxide layer (mill scale) and deep storage rust. If welded over, these impurities get trapped in the molten pool, causing severe porosity and hydrogen cracking. Mechanically grinding scale off thousands of beams is a massive labor drain.
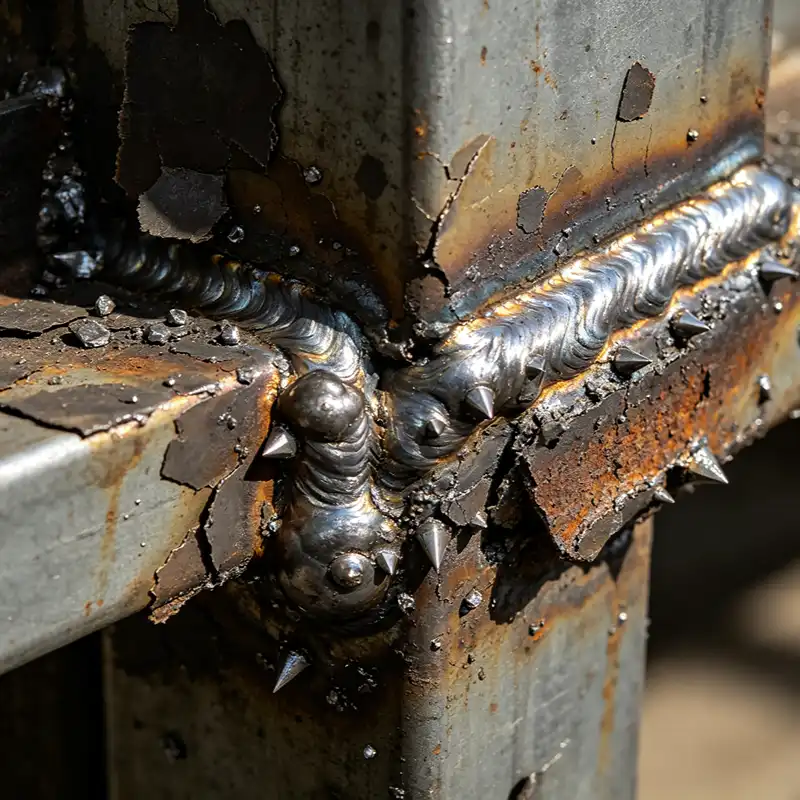
Aggressive Spatter Ruins Powder Coating
Welding thick steel requires high-amperage MIG, which generates violent molten spatter. These sharp metal droplets fuse to the rack uprights. If they aren’t manually chipped off, they protrude through the final powder coating, creating sharp edges that tear warehouse workers’ hands and cause the paint to chip and rust prematurely.
Why Metal Shelving Need laser welding?
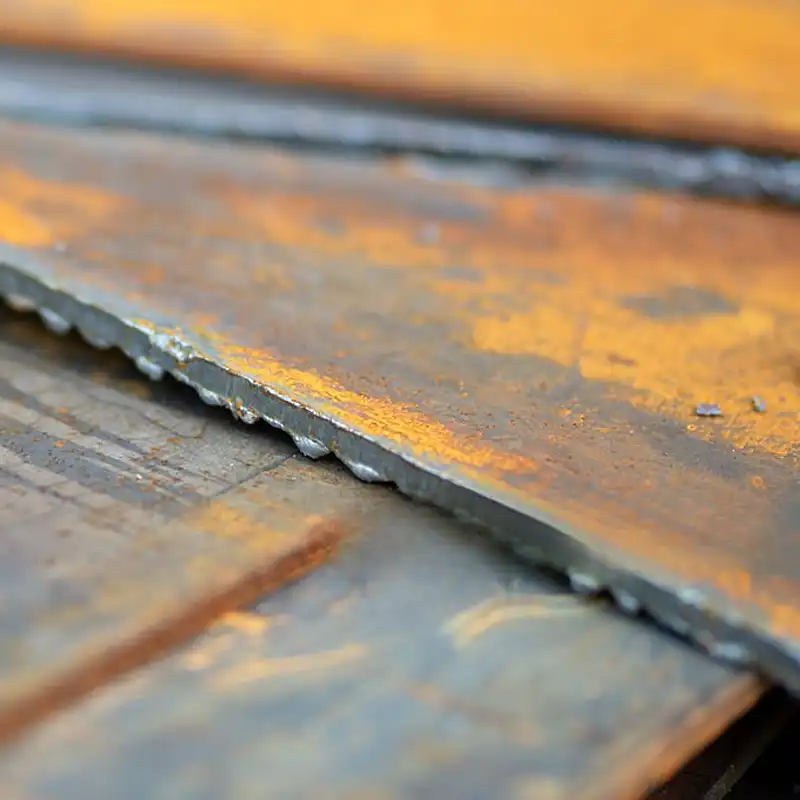
Deep Laser Descaling (Mill Scale Removal)
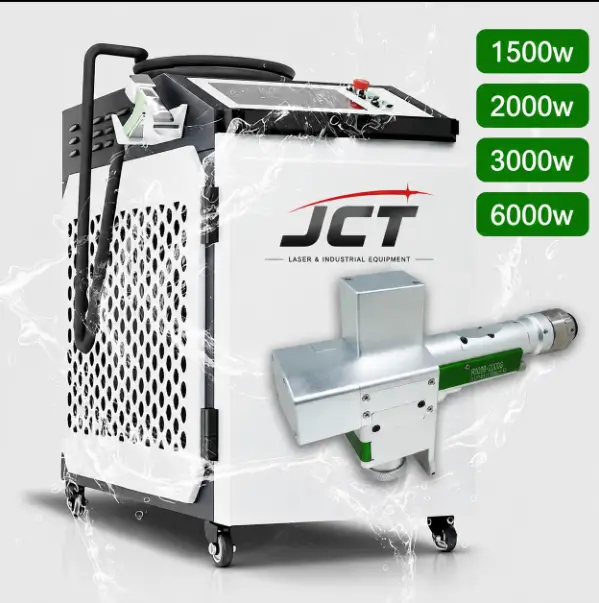
Before welding baseplates to upright columns, use the JCT’s cleaning mode. High-intensity nanosecond pulses instantly blast away thick mill scale, cutting fluids, and deep rust along the joint line. This reveals a perfectly pure metallic substrate, preventing weld porosity without the noise and silica dust of heavy grinding wheels
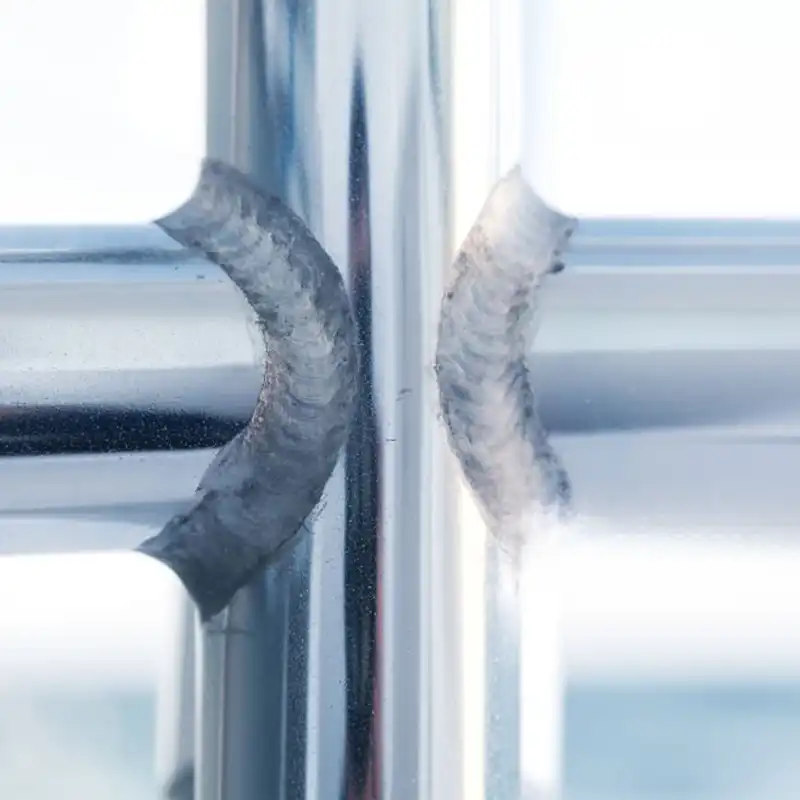
High-Penetration Keyhole Welding
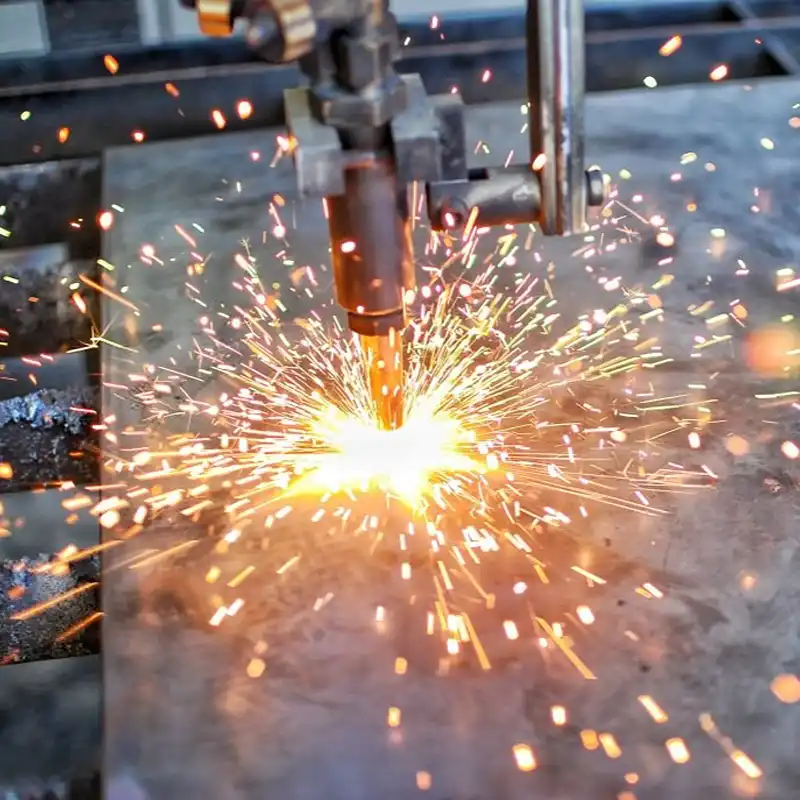
Switch to welding mode utilizing 2000W or 3000W of CW laser power. The beam drills a deep keyhole into the thick carbon steel, fusing 3mm to 6mm plates with a single pass. It travels rapidly, ensuring massive structural strength with zero spatter. Your teardrop connectors and baseplates are welded flawlessly, ready for paint.
Instant Powder Coat Preparation
If any soot or minor oxidation remains around the weld zone, a quick 2-second pass with the laser cleaning mode can eradicate it. The steel racking components proceed directly to the powder coating oven with a pristine, Sa 3.0 purity level, guaranteeing heavy-duty paint adhesion for industrial environments.
Laser Solutions for Shelving Fabricators
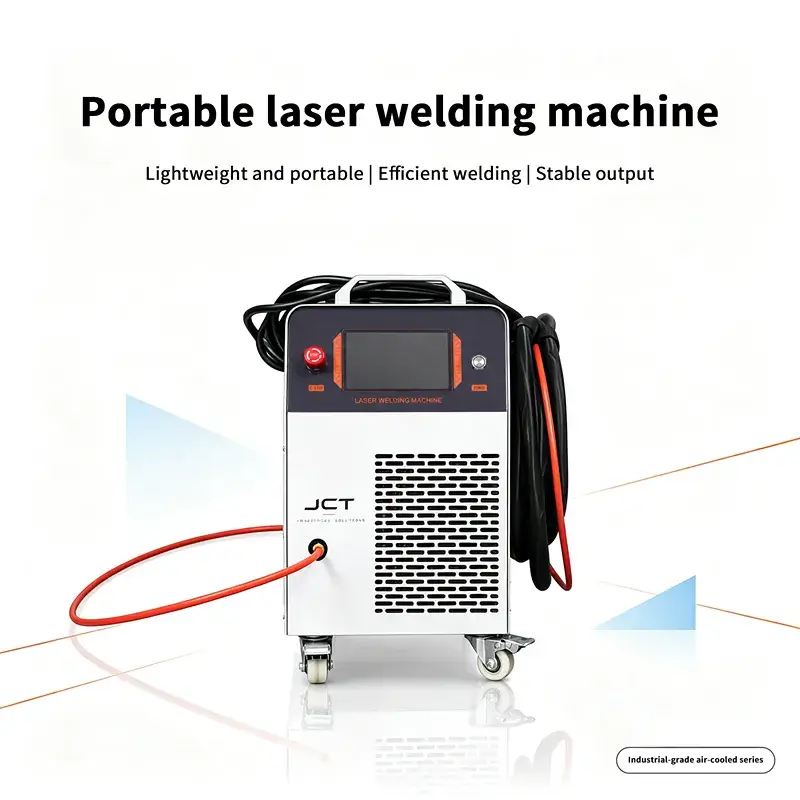
- Custom cantilever racks, mezzanine staircases, and specialized material handling carts.
Easily penetrates 4mm to 6mm carbon steel. Eradicates the massive spatter cleanup associated with MIG welding. The built-in cleaning mode effortlessly blasts away deep mill scale from raw structural steel before assembly.
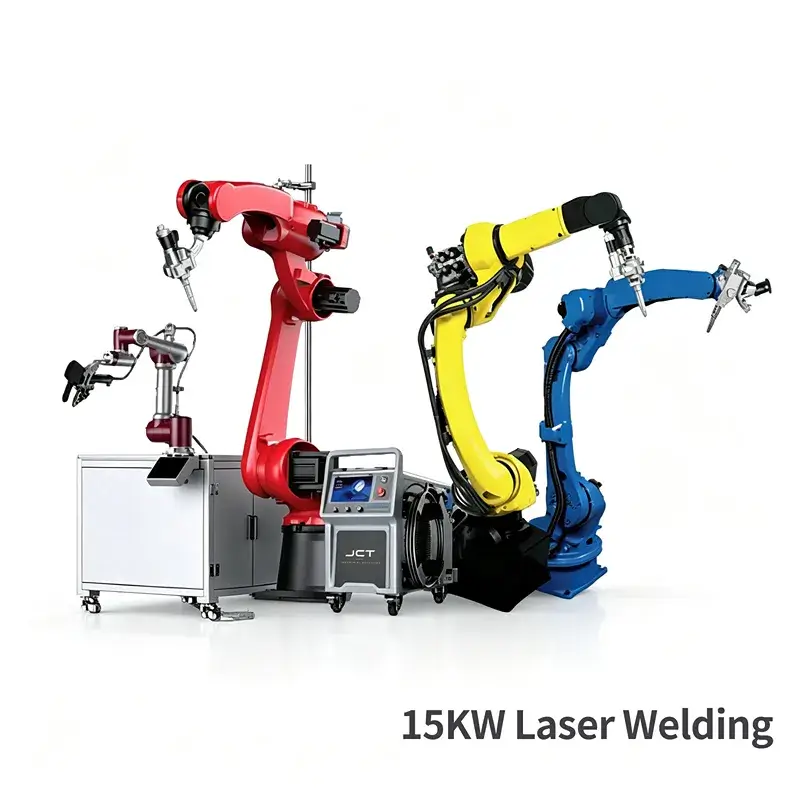
High-volume production of standard teardrop beams, upright columns, and baseplate attachments.
Integrates high-power lasers with heavy-payload 6-axis robotics. Delivers relentless, identical, full-penetration welds on massive racking components 24/7. Completely eliminates the human fatigue of maneuvering heavy MIG guns, ensuring consistent RMI load-rating compliance on every single beam.
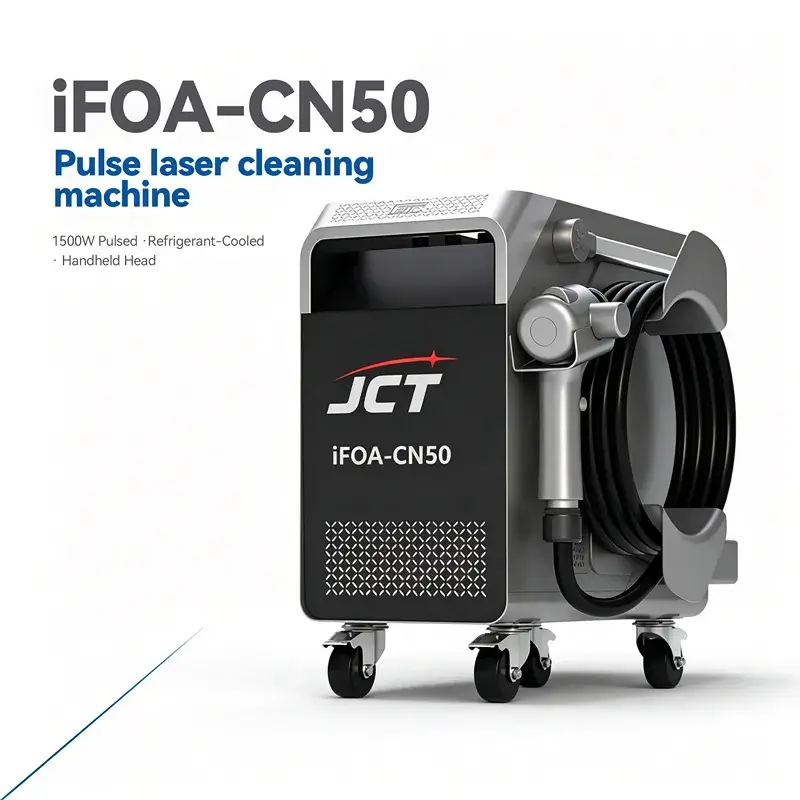
Restoring rusted steel inventory and prepping massive structural components for heavy-duty powder coating.
Uses high-energy heat to instantly strip stubborn mill scale and heavy storage rust without abrasive wheels. Ensures an Sa 3.0 pristine surface, guaranteeing that industrial powder coats adhere flawlessly to withstand severe warehouse impacts.
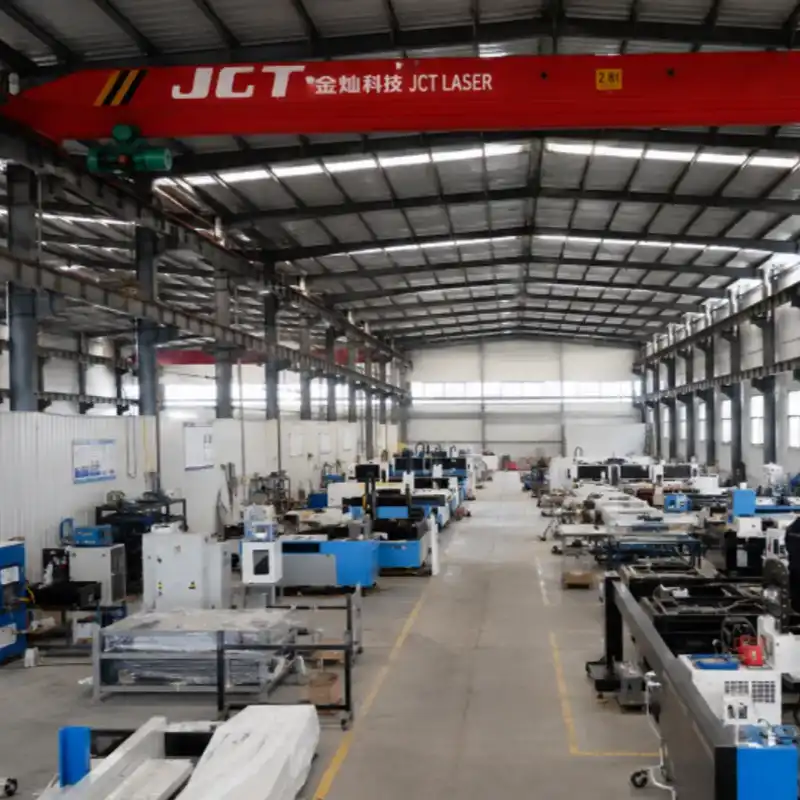
WHO WE ARE?
Manufacturingthe Future of Laser Fabrication & Quality Control.
With over 10 years of industry expertise, we have grown into a trusted source for industrial laser welding & fabrication processing systems and precision environmental testing equipment.
At JCT, we not only build machines; but also build reliability.
From rapid metal fabrication to simulating extreme -40°C climates for your material testing,we ensure every set of equipment meets strict global standards.
We are committed to accelerating your R&D cycles and safeguarding your brand’s reputation with robust, factory-direct solutions.
SUCCESS CASES
Trusted by Manufacturers Worldwide
From streamlining sheet metal production lines to ensuring automotive sensor components pass rigorous high- and low-temperature and humidity environmental tests, our solutions are helping customers around the world boost production efficiency and improve quality. Learn how we help our customers overcome their toughest manufacturing and testing challenges.
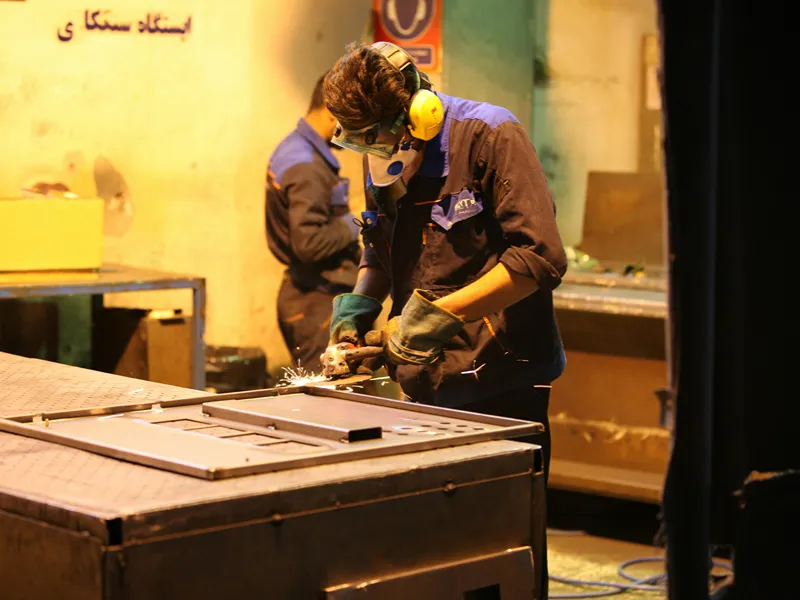
Discover how an Australian manufacturer used our laser solutions to solve the problem of recruiting skilled welders and completely eliminate the need for post-welding secondary grinding
See how a Tier-2 supplier from North America used our temperature shock chamber to pass strict automotive certifications and secure a global contract
Learn how an electrical cabinet manufacturer from Dubai ,used our industrial laser welders to eliminate weld spatter and thermal distortion, then their electrical cabinet products achieved a 100% first-pass yield rate and successfully passed IP66 outdoor certification.
Learn how a Southeast Asian smart home brand used our environmental chamber to conduct accelerated aging tests, optimize PCB coatings, and significantly reduce their global return rate.
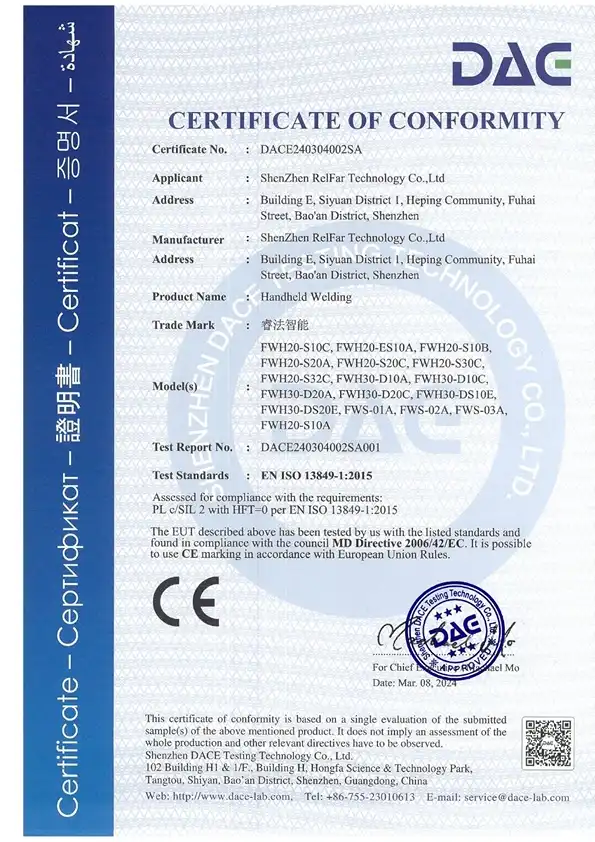
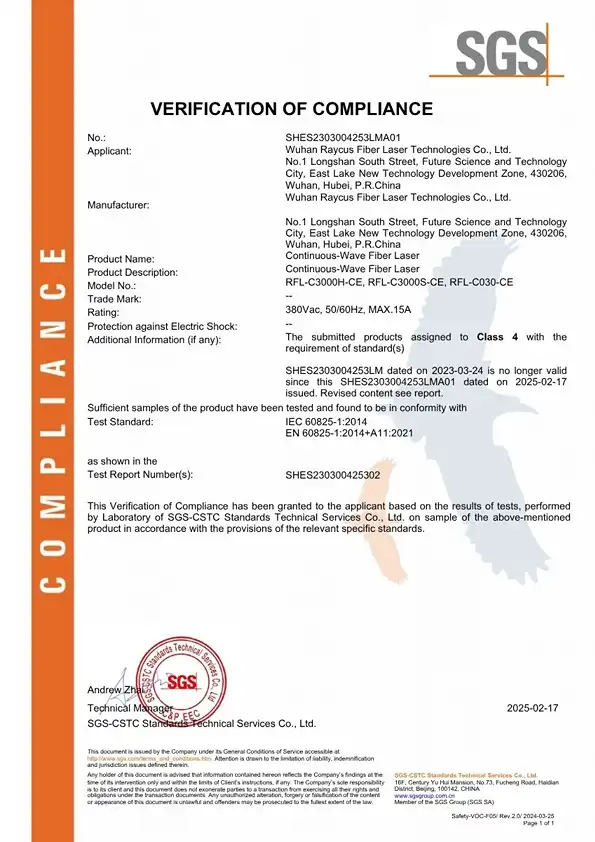
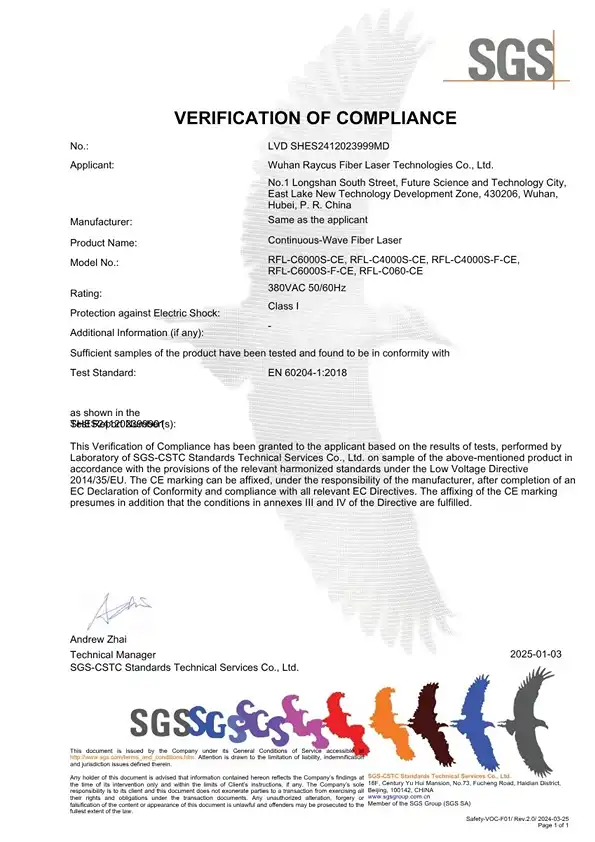
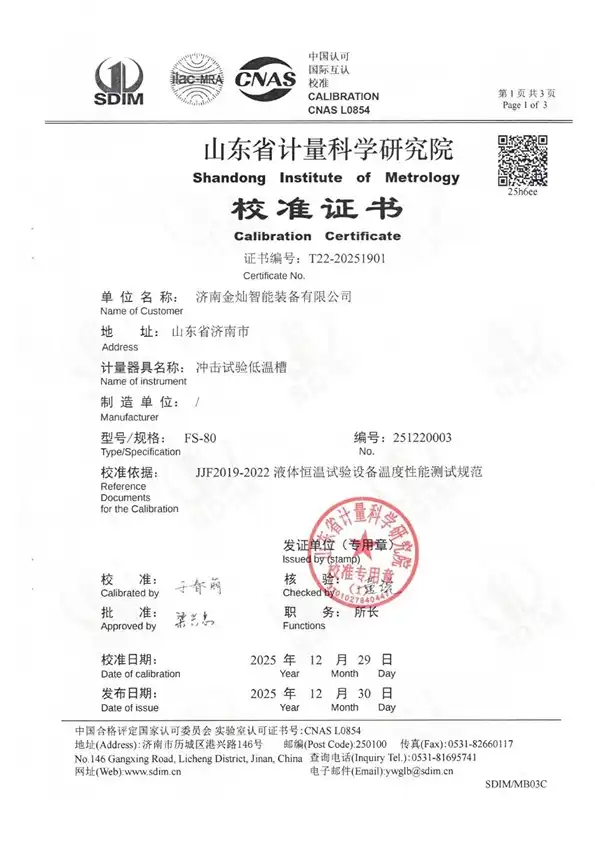
PREMIUM COMPONENTS ASSURANCE
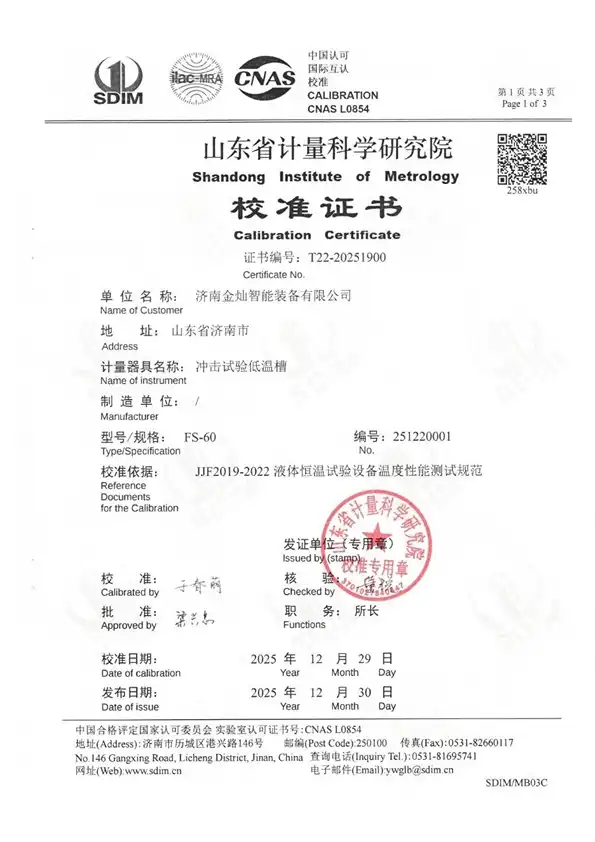
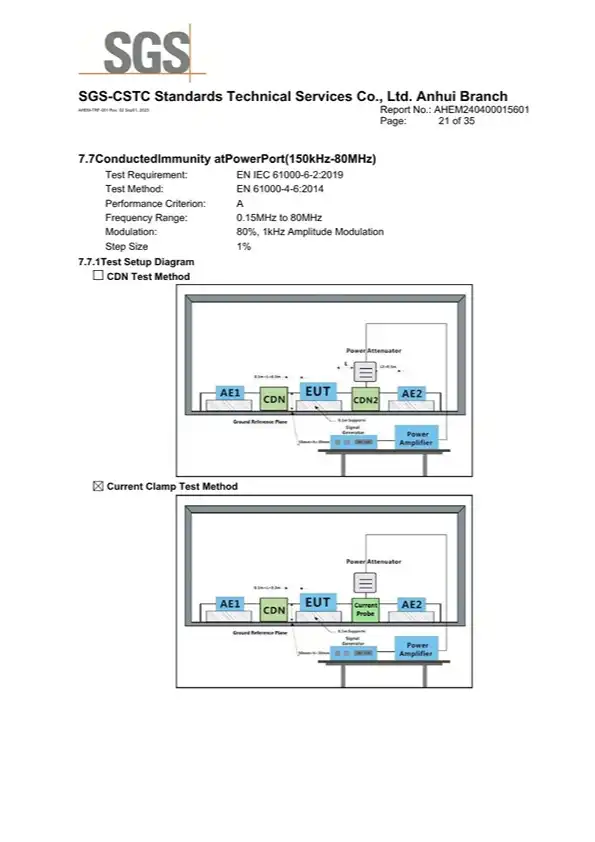
Certified to Global Leading Standards
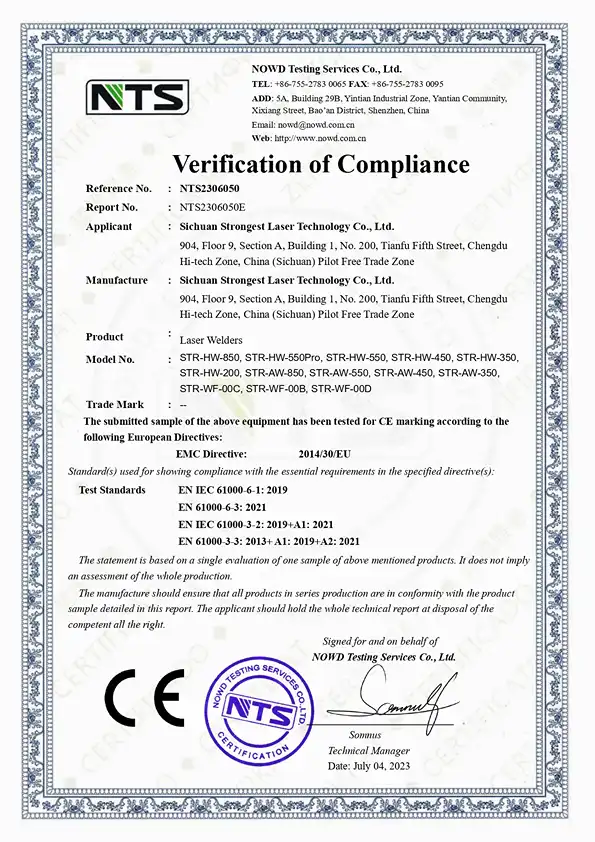
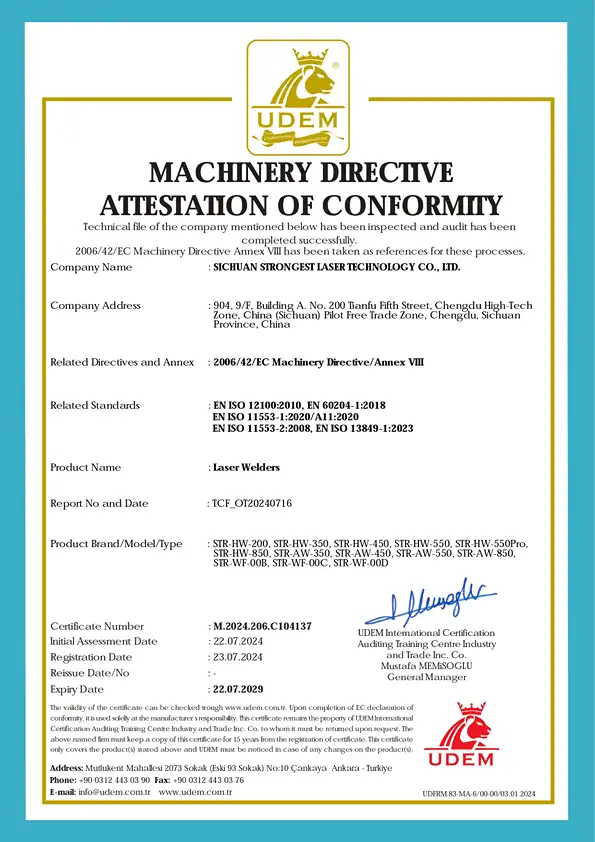
Reliability starts at the core. The key components that power our equipment—from the laser source to even the smallest electronic components—have all been certified to meet the world’s most stringent international standards.
GLOBAL PARTNERSHIPS
Trusted by Industry Leaders Worldwide
We take pride in powering the success of top-tier global manufacturers, research institutions, and industrial leaders. Our advanced laser and testing solutions are trusted worldwide to deliver uncompromising quality and peak performance.
FAQ
Q1: We waste massive amounts of time chiseling MIG spatter off rack uprights before painting. Does laser fix this?
Absolutely.
MIG generates turbulent molten spatter that fuses to the steel. But Laser welding utilizes a highly focused beam of light to create a stable keyhole melt pool. The process is virtually 100% spatter-free. Your teardrop beams and uprights can go directly to the powder coating line with zero manual chipping.
Q2: We use thick hot-rolled steel with heavy mill scale. Can the laser weld right through it?
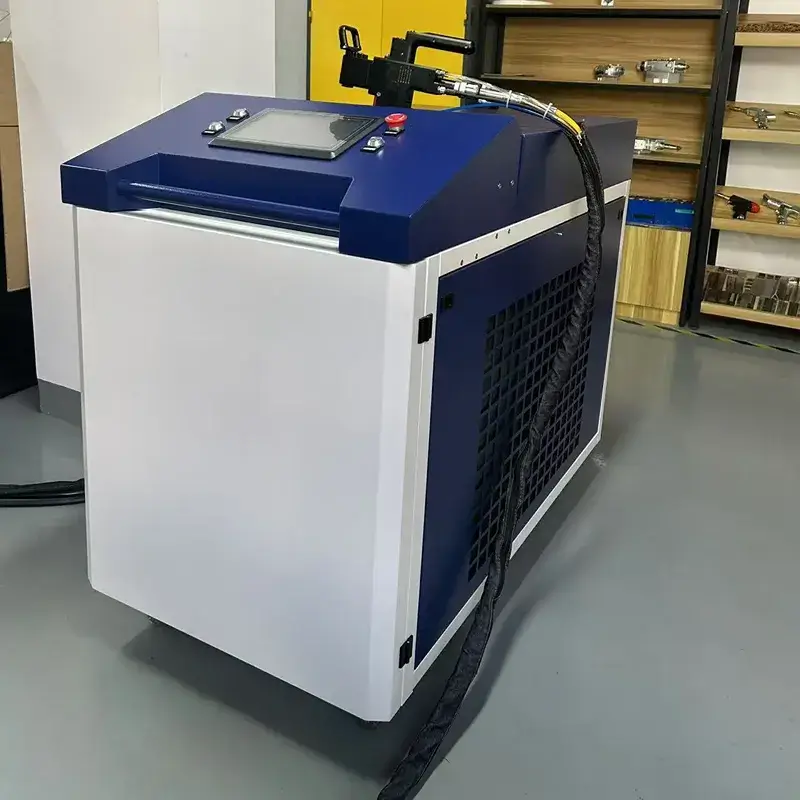
Welding directly over thick mill scale causes porosity, regardless of the method. However, the JCT 5-in-1 system solves this natively. Switch to “Cleaning Mode” to instantly blast away the mill scale along the weld track in seconds, then switch back to welding for a flawless, structurally sound joint.
Q3: What thickness of structural steel can a handheld laser realistically weld?
For heavy-duty shelving, we recommend our 2000W or 3000W handheld laser welders. A 3000W JCT laser can comfortably achieve full single-pass penetration on 6mm (approx. 1/4 inch) carbon steel. If welding thicker baseplates (e.g., 8mm to 10mm), an automated robotic setup provides immense structural strength.
Q4: What shielding gas is required for welding carbon steel racking?
For carbon steel, excellent results can be achieved using a mixture of argon and carbon dioxide (typically 80/20 or a similar standard MIG welding gas) or pure nitrogen. Producing nitrogen in-house using a nitrogen generator is a very cost-effective solution.
Q5: How difficult is it to train our heavy-equipment welders to use the laser?
It is remarkably easy. Because the JCT laer system automatically controls the penetration depth and wire feed speed, the operator simply guides the torch along the seam. Welders accustomed to heavy MIG guns will find the lightweight laser torch reduces fatigue immensely, mastering it within hours.
Q6: What safety enclosures are required for welding large structural racks?
The operator must wear the required laser safety goggles and standard heavy-duty protective gear.
Q7: What is the expected ROI for a heavy-duty shelving manufacturer?
Manufacturers typically see an ROI within 6 to 9 months. This is driven by eliminating the immense labor cost of chipping spatter, removing the grinding bottleneck before powder coating, accelerating welding speeds by up to 300%, and eliminating structural rework caused by incomplete root fusion.
Related Products
Get a Factory-Direct Custom Quote
Stop wasting labor on chipping MIG spatter and grinding mill scale.
Tell our application engineers about your specific structural steel thicknesses, load-bearing requirements, and current fabrication bottlenecks. We will recommend the exact high-power JCT laser configuration to upgrade your racking production line, complete with a factory-direct quote within 12 hours