Hermetic Laser Welding & Cleaning for Electrical Cabinet
JCT offers a one-stop laser processing solution that enables flawless, pore-free joining on galvanised electrical cabinets, server racks and distribution boxes. This completely eliminates panel warping and avoids the laborious secondary grinding process.
The Fabrication Challenge
Fabricating electrical cabinets, telecom enclosures, and power distribution boxes requires joining large, flat panels of thin-gauge carbon steel, stainless steel, or galvanized sheet (1.2mm to 2.5mm).
Traditional MIG and TIG welding consistently threaten the structural and environmental integrity of these enclosures
Panel Warpage Destroys Door Seals
Electrical cabinets rely on perfectly flat surfaces so that rubber gaskets can form a waterproof seal against the doors. Arc welding pumps massive, uncontrolled heat into the thin sheet metal. This causes violent thermal expansion, leaving the cabinet walls buckled and wavy. A warped cabinet means a compromised seal, rendering the enclosure useless for outdoor or industrial environments.
Pinhole Leaks and IP Rating Failures
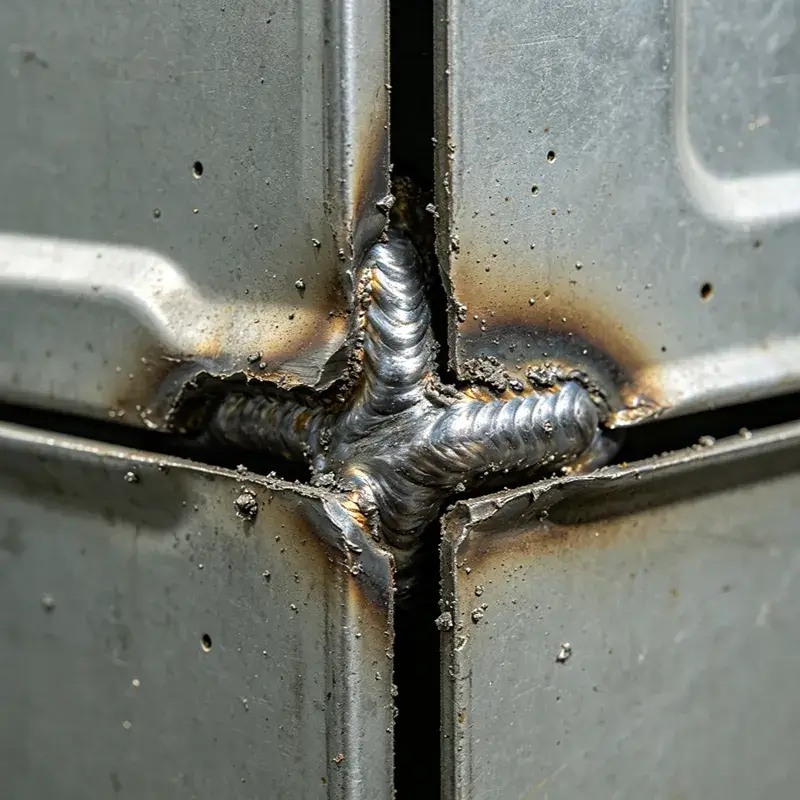
Manual MIG welding often suffers from start/stop defects, cold laps, and zinc outgassing (when welding galvanized steel). These defects create microscopic pinholes in the weld seam. In outdoor telecom cabinets or washdown environments, these pinholes allow moisture ingress, leading to catastrophic short circuits in the enclosed high-voltage electrical components.
Grinding Destroys Corrosion Protection
MIG welding leaves a bulky, spatter-covered crown. Fabricators must aggressively grind these seams flat to accommodate hinges or achieve a clean aesthetic. Grinding not only thins the structural corner but entirely strips away the factory galvanized zinc coating, creating an immediate focal point for rust and corrosion once deployed in the field.
Why Electrical Cabinet Need laser welding?
Pre-Weld Zinc Ablation (Surface Prep)
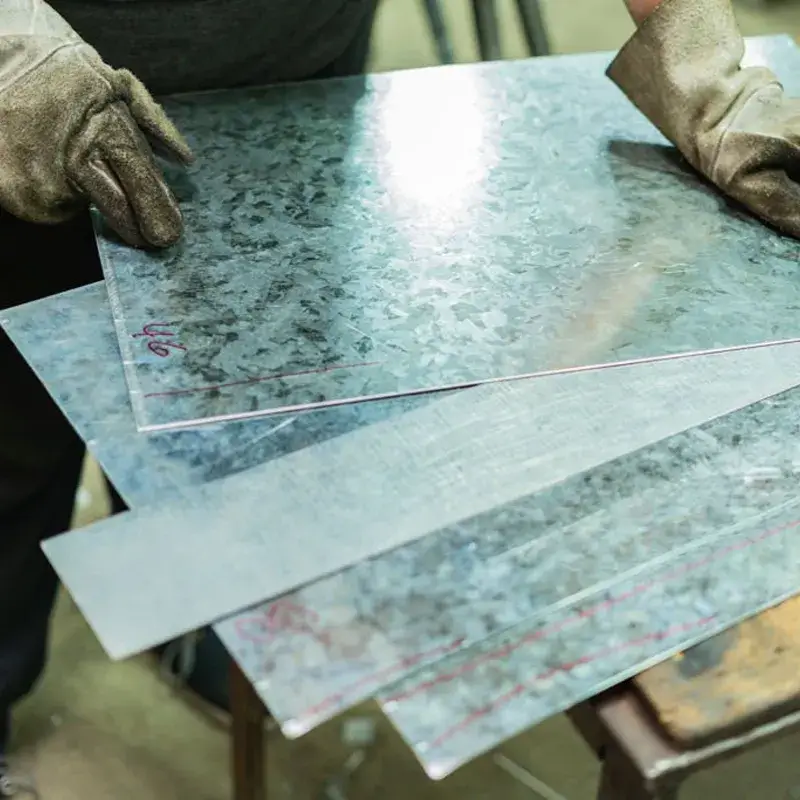
When fabricating galvanized distribution boxes, zinc outgassing causes severe weld porosity. Using the JCT cleaning mode, operators vaporize a 2mm track of zinc exactly along the intended weld seam. This leaves the surrounding protective galvanization perfectly intact while providing a pure bare-steel track for a high-strength, hermetic weld.
Low-Heat Hermetic Welding
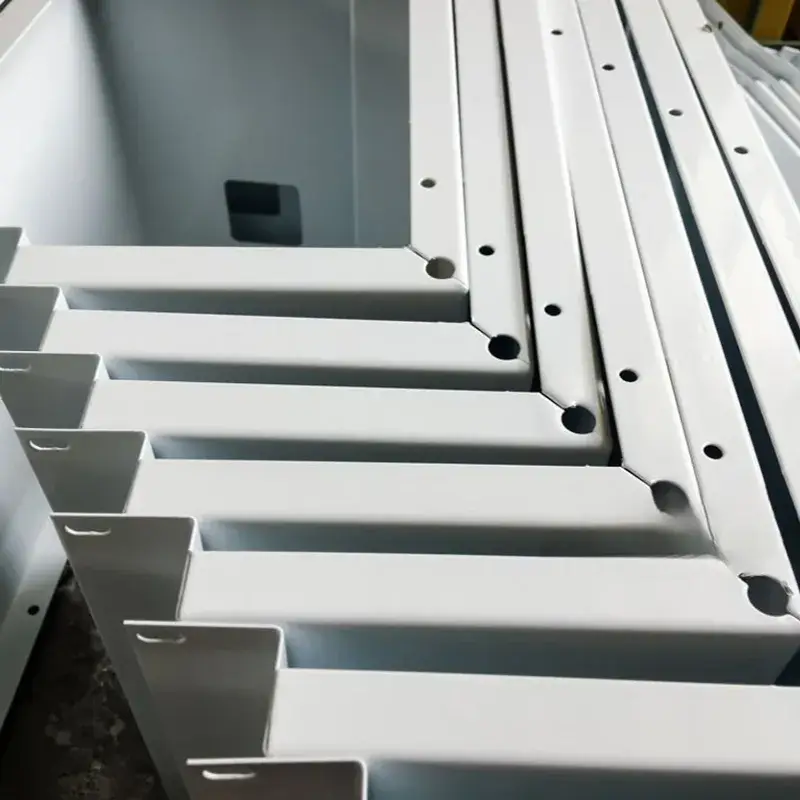
Switch to welding mode to join the cabinet walls and roof. The CW laser penetrates instantly, traveling up to 4x faster than MIG. The localized heat input guarantees that the massive 2-meter cabinet side panels remain perfectly flat, ensuring your rubber door gaskets will seat flawlessly. The resulting corner weld is so smooth it requires zero abrasive grinding
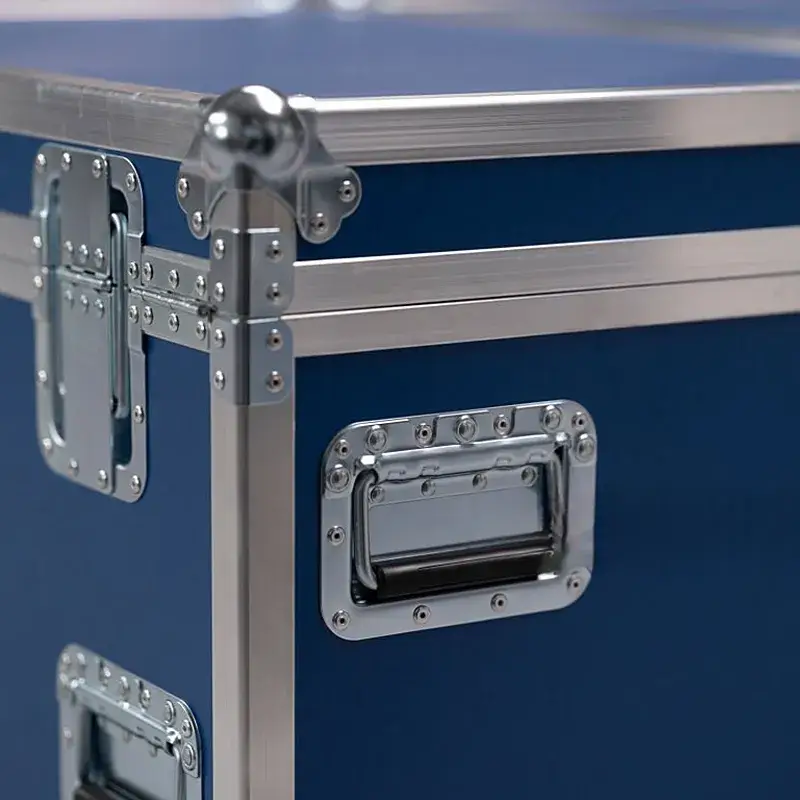
Instant Surface Prep for Earthing/Coating
Grounding (earthing) studs require perfect electrical conductivity. Switch back to cleaning mode to instantly ablate any minor oxidation or residual oils from the weld zone or the grounding points. The cabinet can immediately be moved to the powder coating line, completely bypassing loud, dusty, and labor-intensive grinding stations.
Laser Solutions for Enclosure Manufacturers
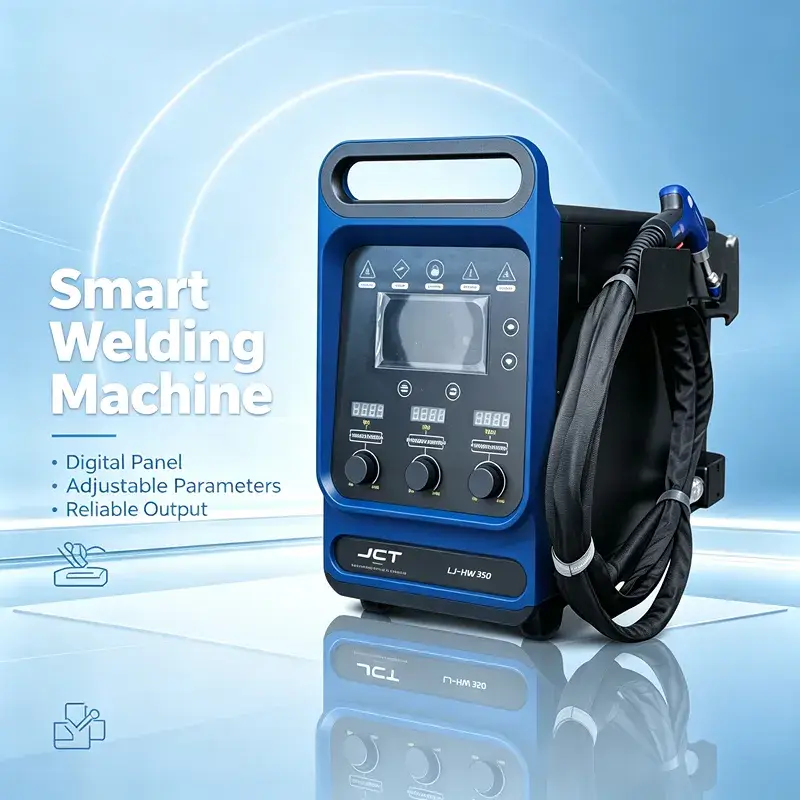
Custom NEMA control panels, bespoke telecom cabinets, and complex low-volume distribution boxes.
Ideal tool for custom enclosure shops. It allows operators to effortlessly weld flush outside corners without causing spatter that ruins the aesthetic. The rapid switch to cleaning mode means raw steel frames are instantly prepped for powder coating, eliminating the need for angle grinders that thin the structural corners.
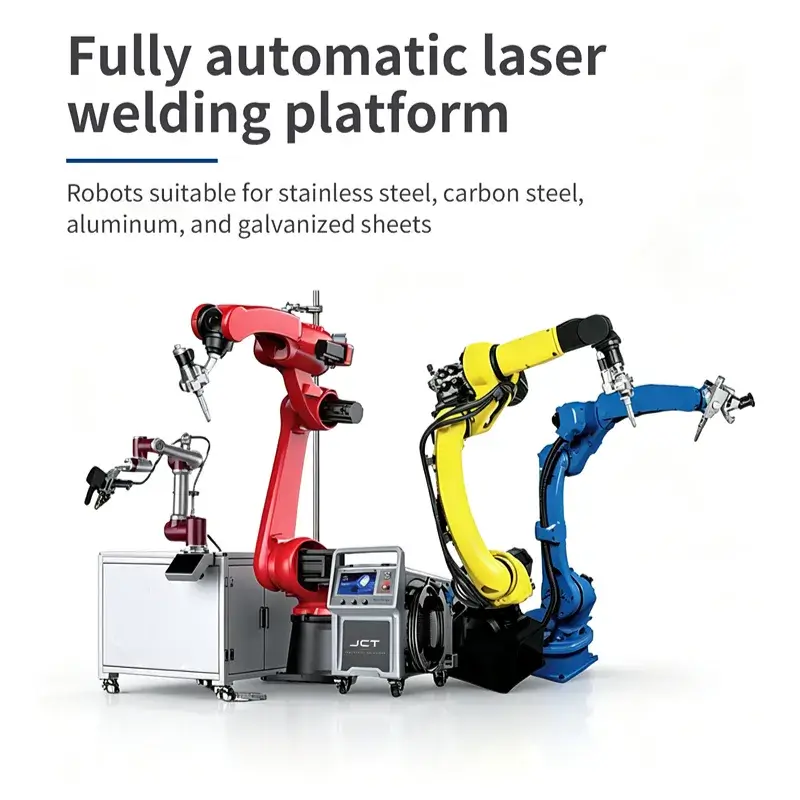
High-volume production of standardized server racks, modular switchgear cabinets, and mass-produced electrical housings.
Integrates our continuous wave (CW) lasers with large-format 6-axis robotics for relentless mass production. It delivers flawless, identical, IP66-rated joints on thousands of cabinets 24/7. Eradicates manual inconsistencies, ensuring every enclosure passes leak testing right off the line.
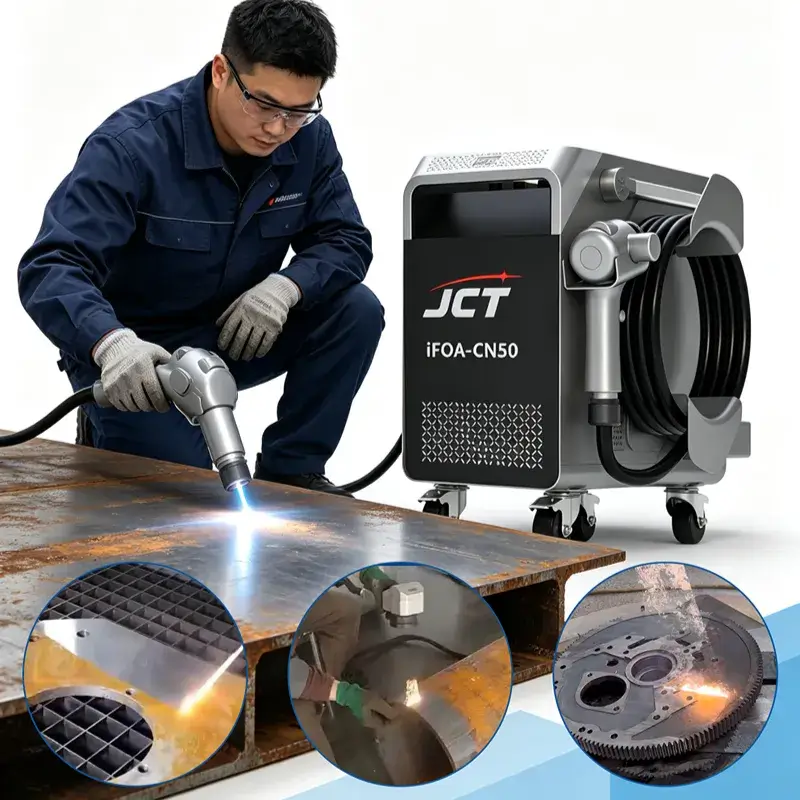
Pre-weld zinc ablation on galvanized sheets and precision cleaning of internal grounding (earthing) points
Uses nanosecond pulses to cleanly blast away zinc or oxidation specifically where electrical conductivity is required. It provides a purely metallic substrate for critical grounding stud welds without damaging the surrounding protective galvanization or scratching the metal
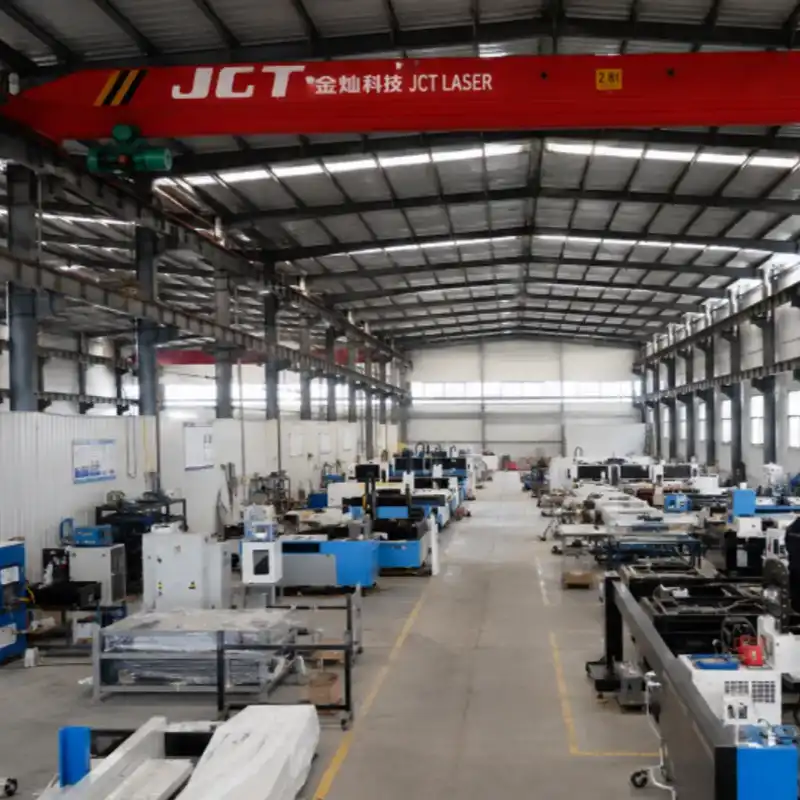
WHO WE ARE?
Manufacturingthe Future of Laser Fabrication & Quality Control.
With over 10 years of industry expertise, we have grown into a trusted source for industrial laser welding & fabrication processing systems and precision environmental testing equipment.
At JCT, we not only build machines; but also build reliability.
From rapid metal fabrication to simulating extreme -40°C climates for your material testing,we ensure every set of equipment meets strict global standards.
We are committed to accelerating your R&D cycles and safeguarding your brand’s reputation with robust, factory-direct solutions.
SUCCESS CASES
Trusted by Manufacturers Worldwide
From streamlining sheet metal production lines to ensuring automotive sensor components pass rigorous high- and low-temperature and humidity environmental tests, our solutions are helping customers around the world boost production efficiency and improve quality. Learn how we help our customers overcome their toughest manufacturing and testing challenges.
Discover how an Australian manufacturer used our laser solutions to solve the problem of recruiting skilled welders and completely eliminate the need for post-welding secondary grinding
See how a Tier-2 supplier from North America used our temperature shock chamber to pass strict automotive certifications and secure a global contract
Learn how an electrical cabinet manufacturer from Dubai ,used our industrial laser welders to eliminate weld spatter and thermal distortion, then their electrical cabinet products achieved a 100% first-pass yield rate and successfully passed IP66 outdoor certification.
Learn how a Southeast Asian smart home brand used our environmental chamber to conduct accelerated aging tests, optimize PCB coatings, and significantly reduce their global return rate.
PREMIUM COMPONENTS ASSURANCE
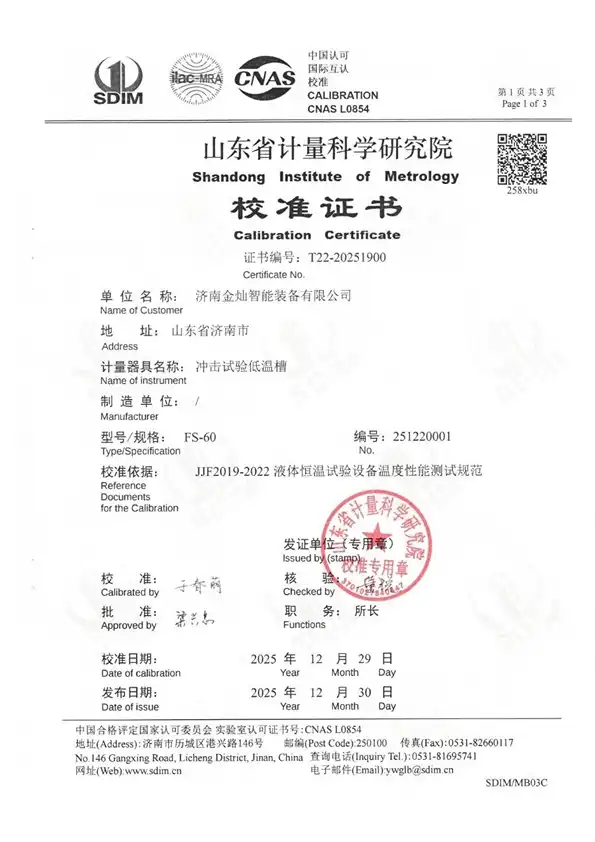
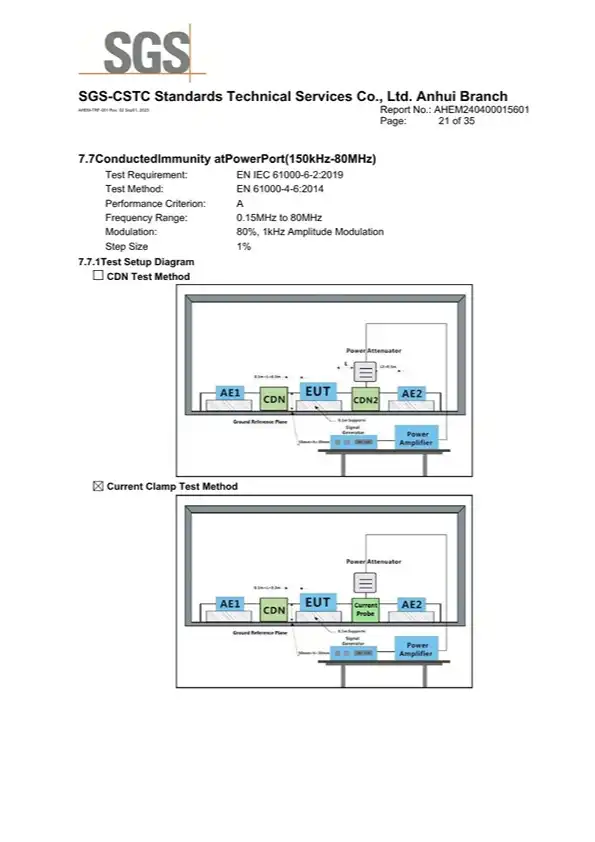
Certified to Global Leading Standards
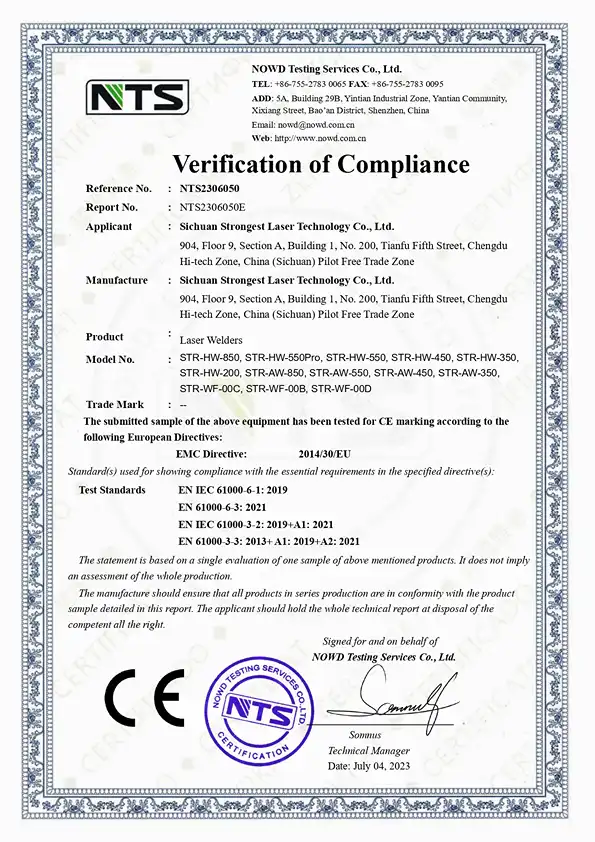
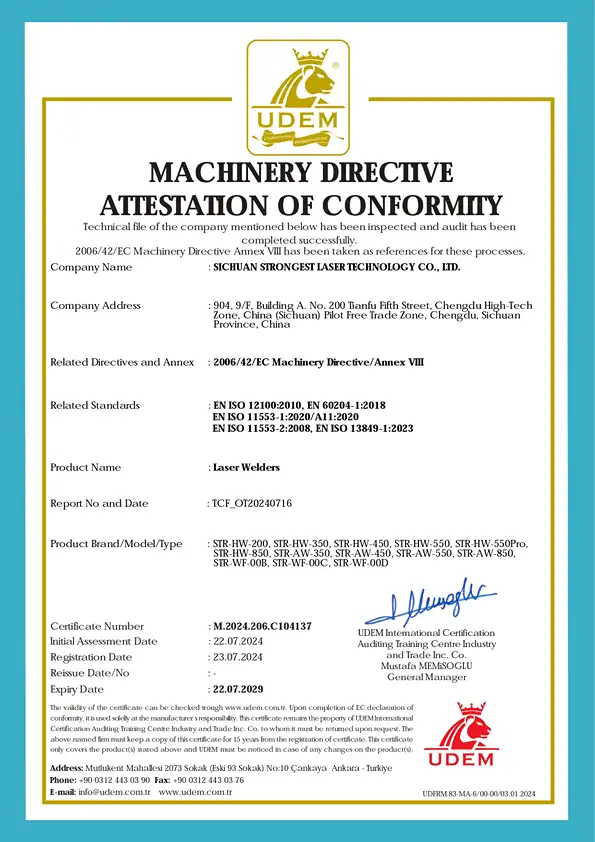
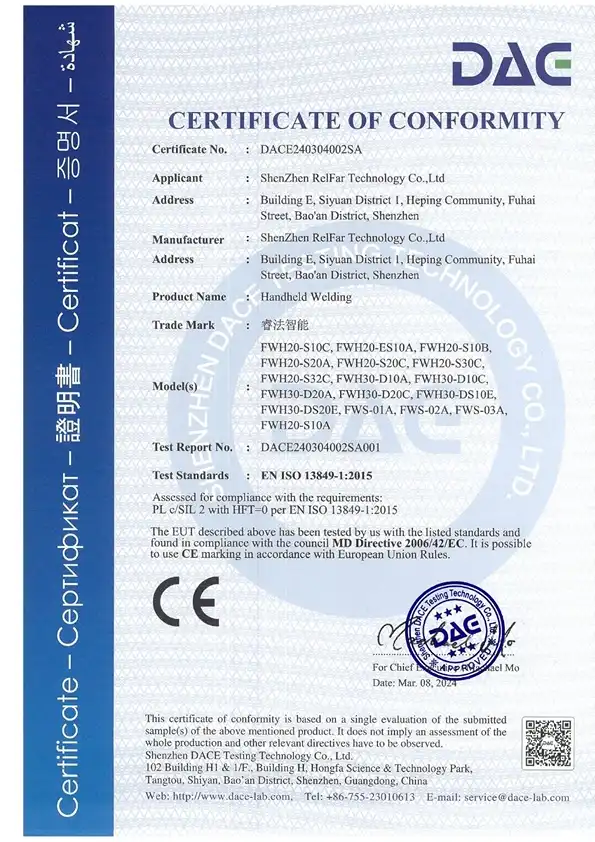
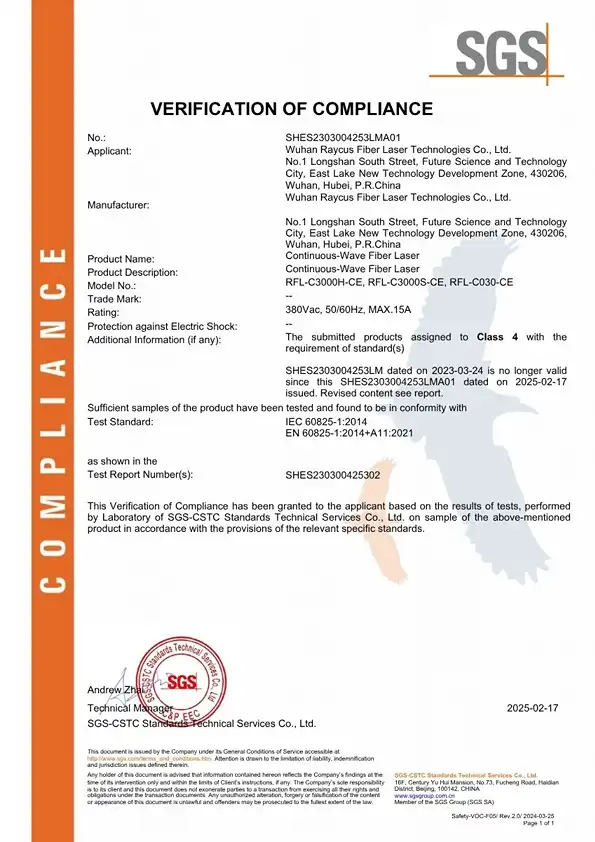
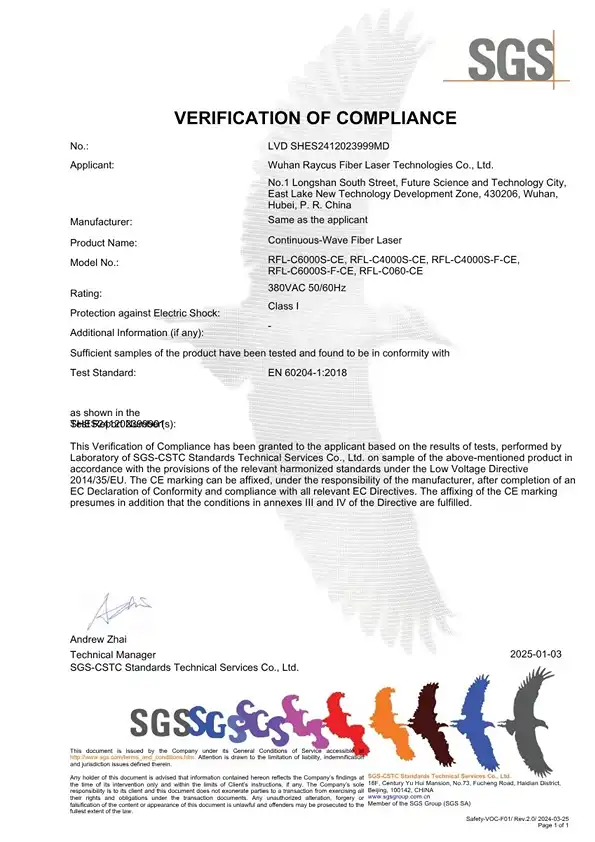
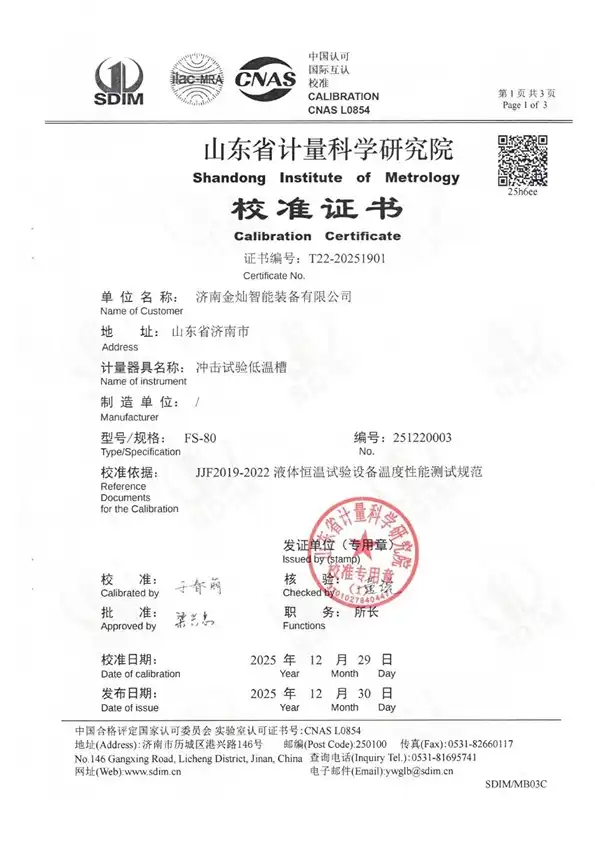
Reliability starts at the core. The key components that power our equipment—from the laser source to even the smallest electronic components—have all been certified to meet the world’s most stringent international standards.
GLOBAL PARTNERSHIPS
Trusted by Industry Leaders Worldwide
We take pride in powering the success of top-tier global manufacturers, research institutions, and industrial leaders. Our advanced laser and testing solutions are trusted worldwide to deliver uncompromising quality and peak performance.
FAQ
Q1: We weld large 1.5mm control panel doors, and they always warp. Will a laser fix this?
Yes, definitively. MIG and TIG transfer heat too slowly, it will flood the entire panel and cause violent thermal expansion. Fiber lasers melt a microscopic spot instantly, and the metal cools before the heat can travel. The Heat Affected Zone (HAZ) is fractions of a millimeter wide, guaranteeing your massive 1.5mm doors remain perfectly flat and seal tightly against their gaskets.
Q2: We struggle to pass IP65 leak tests because of pinholes in our MIG welds. How does laser compare?
Laser welding is vastly superior for environmental sealing. Because the laser creates a continuous, high-density keyhole weld .It is stabilized by the machine’s optics, it eliminates the start/stop defects, cold laps, and human-error pinholes common in manual arc welding. A laser weld is naturally hermetic.
Q3: Does welding galvanized steel for outdoor cabinets cause huge spatter and porosity with a laser?
Not with our systems.
Galvanized steel porosity is caused by trapped zinc vapor. JCT lasers utilize a high-frequency “wobble” (oscillation) head. This stirs the weld pool, allowing the zinc vapors to safely exhaust before the steel freezes, resulting in dense, spatter-free, porosity-free joints.
Q4: Can we use the laser to strip the zinc coating only where we intend to weld?
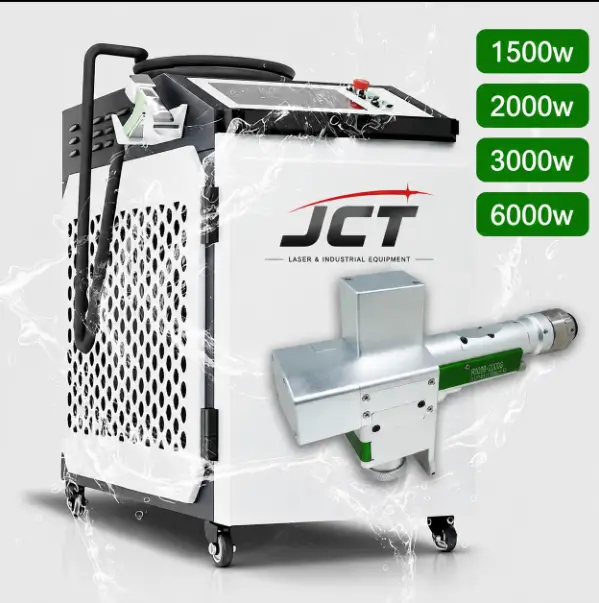
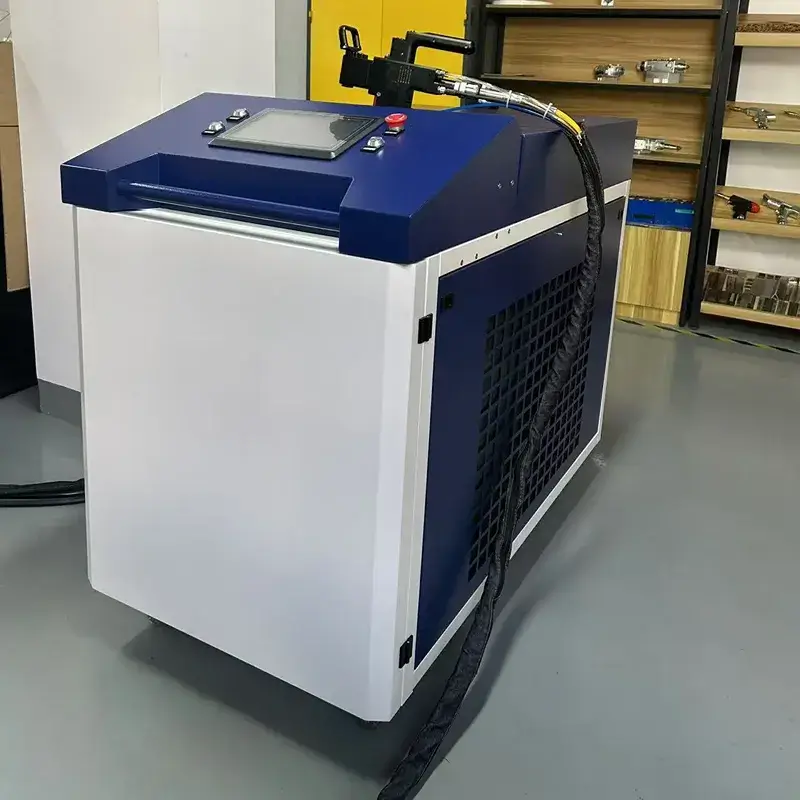
Exactly. The 3-in-1 handheld system switches to “Cleaning Mode” instantly. You can perform a quick pass over the joint edge to ablate a precise 2mm track of zinc. This prevents zinc contamination in the weld pool ,while keeping the rest of the cabinet’s rust-preventative galvanization completely intact.
Q5: We waste hours grinding the outside corners of our enclosures flat for painting. Can laser eliminate this?
Yes.
Laser welding produces an incredibly smooth, narrow, and nearly flush bead on outside corner joints.. If any minor oxidation is present, you just need to use a 2-second pass with the laser cleaning mode preps it perfectly, eliminating abrasive grinding
Q6: Can the laser prepare areas for welding internal electrical grounding (earthing) studs?
Yes.
You can use the laser cleaning mode to instantly vaporize any mill scale, oil, or light rust from the exact spot where the stud will be welded, ensuring perfect electrical conductivity without scratching the sheet metal.
Q7: How difficult is it to train our existing assembly workers to use a handheld laser?
Because the machine controls the heat input, penetration depth, and wire feed rate, the operator relies purely on guiding the nozzle smoothly along the seam. An entry-level assembler with zero prior welding experience can learn to produce flawless, IP-rated enclosure corners in less than an hour.
Q8: What safety setup is required in our enclosure assembly factory?
As Class 4 lasers, you must establish an enclosed welding booth using laser-safe curtains or panels to block invisible scattered light from the rest of the shop floor. The operator must wear the provided wavelength-specific safety goggles and standard protective clothing.
Q9: What is the ROI timeline for an electrical enclosure manufacturer?
Most enclosure manufacturers see a full ROI within 4 to 8 months. This rapid payback is driven by welding up to 4x faster, completely eliminating the labor bottleneck of grinding frame corners, ending the need to mechanically press warped doors, and eliminating scrap caused by failed IP leak tests
Related Products
Get a Factory-Direct Custom Quote
Stop wasting labor on pressing warped doors and grinding MIG spatter off your control panels.
Tell our application engineers about your specific enclosure materials (e.g., galvanized steel, stainless), thicknesses, and required IP/NEMA ratings. We will recommend the exact JCT laser configuration to upgrade your assembly line, complete with a direct factory quote within 12 hours.