Airtight Laser Welding & Cleaning for HVAC Ductwork
JCT’s advanced laser processing solutions enable the production of high-pressure HVAC pipes and ducts with excellent airtightness, completely eliminating issues such as leaks at mechanical joints, toxic bituminous sealants and burn-through of thin sheets; the products comply directly with the SMACNA Class 3+ standard.
The Fabrication Challenge
Manufacturing earthmoving equipment, cranes, and mining machinery requires processing high-tensile structural steel (like S690QL) and wear-resistant steel (like Hardox 450/500) in extreme thicknesses (15mm to 60mm). Traditional HD Plasma and Oxy-fuel cutting create catastrophic production delays
Massive Heat Affected Zones (Degrading Steel Hardness)
Wear-resistant steels derive their strength from highly controlled quenching and tempering at the mill. Oxy-fuel and plasma blast the metal with uncontrolled, wide-spreading heat. This creates a massive Heat Affected Zone (HAZ) that anneals the edge, stripping the steel of its hardness and reducing the lifespan of excavator buckets and bulldozer blades.
Edge Taper and Heavy Dross (The Milling Bottleneck)
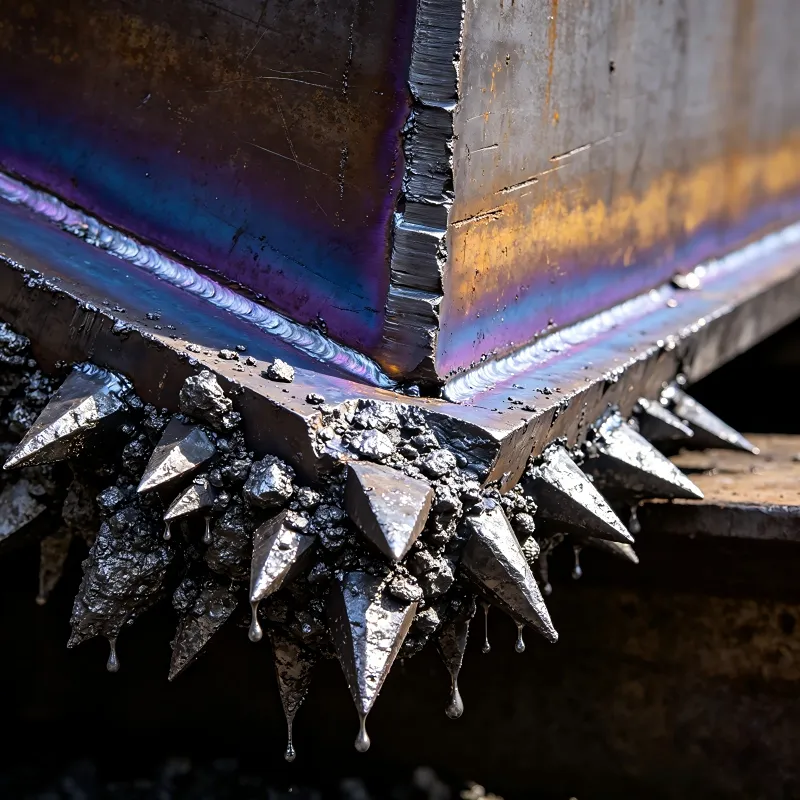
Plasma arcs inherently bow as they cut deeper, creating a tapered (V-shaped) edge rather than a perfectly perpendicular 90-degree face. Additionally, they will leave thick, hardened slag (dross) on the bottom edge. Fabricators have to move these massive plates to heavy CNC milling machines or use laborers with aggressive grinders to square the edges and remove slag before welding
The Secondary Beveling effect
Thick plates require V, Y, or K bevels for full-penetration structural welds. Cutting the part on a plasma table, then moving it via overhead crane to a mechanical beveling machine, and setting up the cut angle takes hours per piece, crippling factory throughput
Why Construction Equipment Need laser cutting?
High-Speed Thick Plate Profiling (12kW - 60kW)
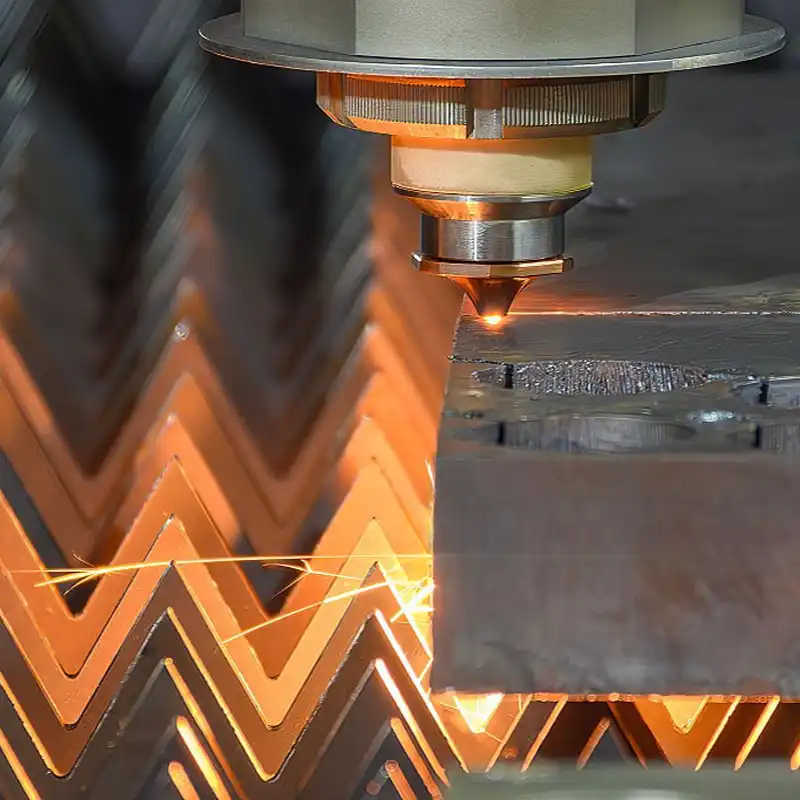
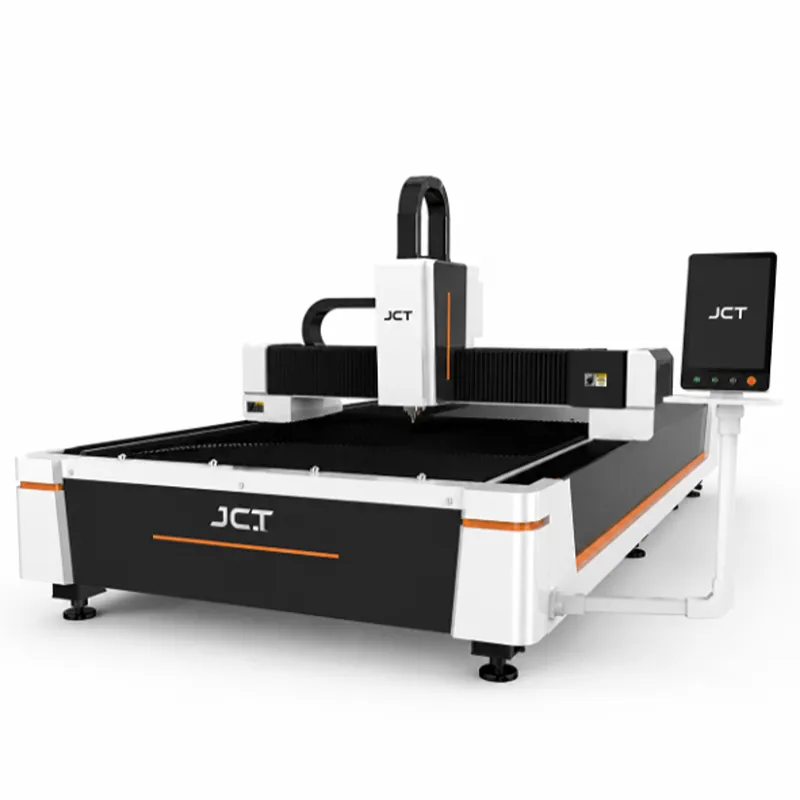
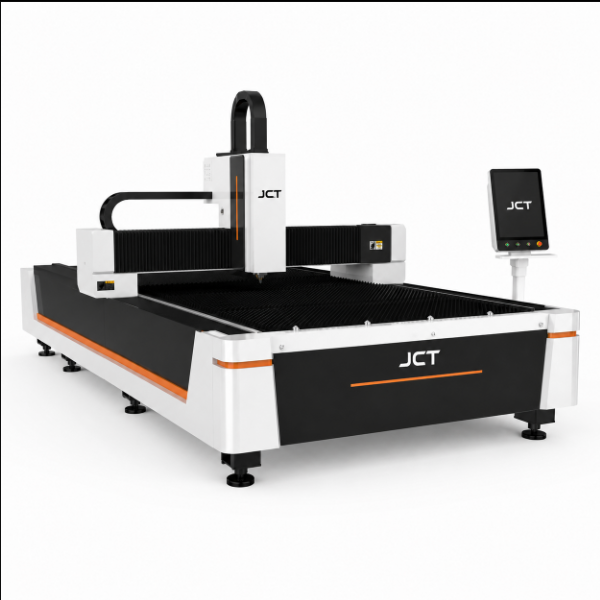
Utilizing JCT’s ultra-high-power flatbed lasers,you can slice through 30mm carbon steel or Hardox plates. Unlike plasma, the laser maintains a perfectly perpendicular, dross-free edge. The incredibly narrow kerf minimizes material waste, allowing tighter nesting of complex chassis parts and boom side-plates.
Single-Setup 3D Bevel Cutting
Equipped with a 5-axis cutting head, the JCT laser performs straight cuts and complex bevels (up to 45 degrees) in the same program. It effortlessly produces V-bevels, Y-bevels, and countersunk holes on heavy plates. The part leaves the machine completely prepped for structural welding, entirely bypassing the heavy machining department.
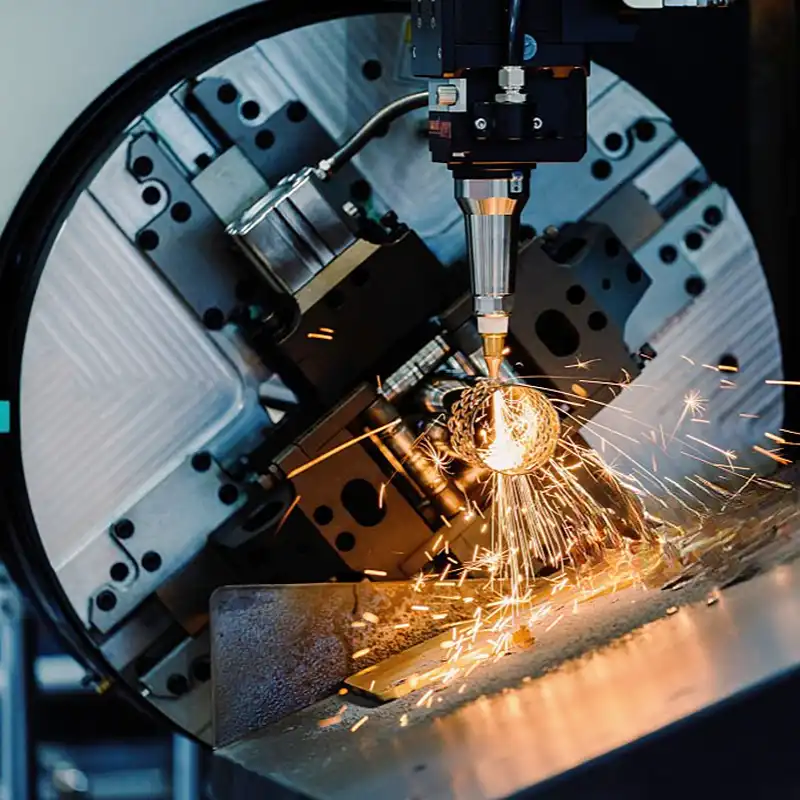
Heavy Tube & Profile Cutting
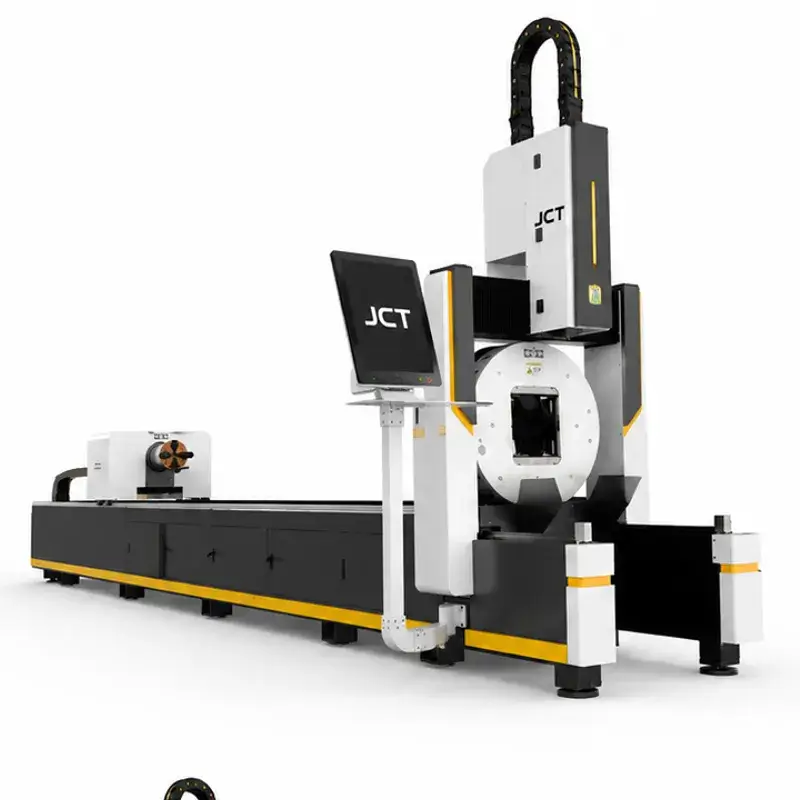
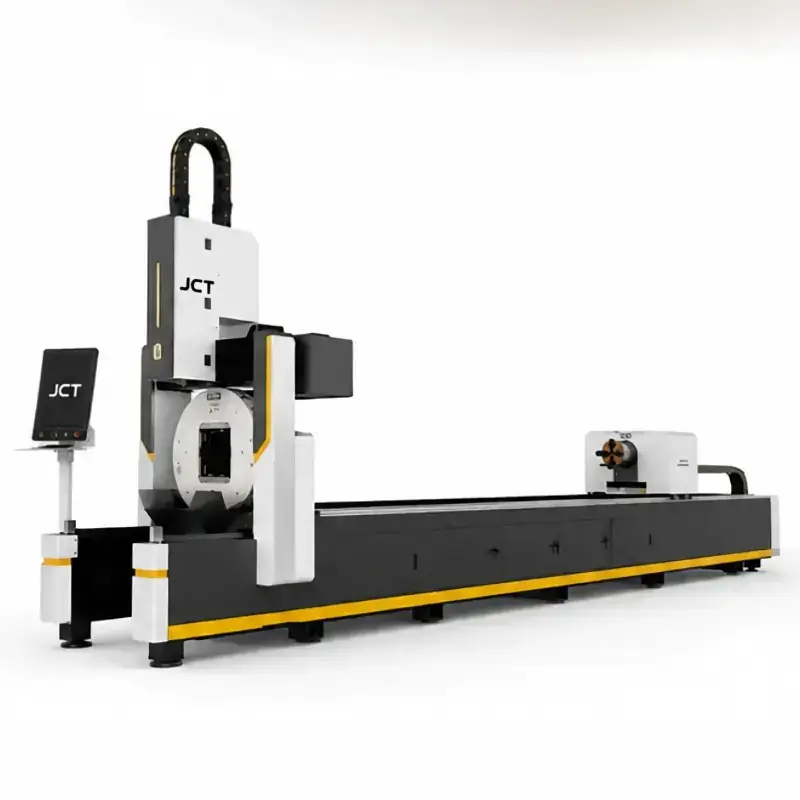
Switch to the JCT Heavy Duty Tube Laser for processing square, rectangular, and H-beams used in the main frame and ROPS cabins. The machine automatically loads heavy profiles, cuts intersecting fish-mouth joints, slots, and holes in one continuous operation, eliminating manual sawing, drilling, and coping.
Laser Solutions for Heavy Machinery
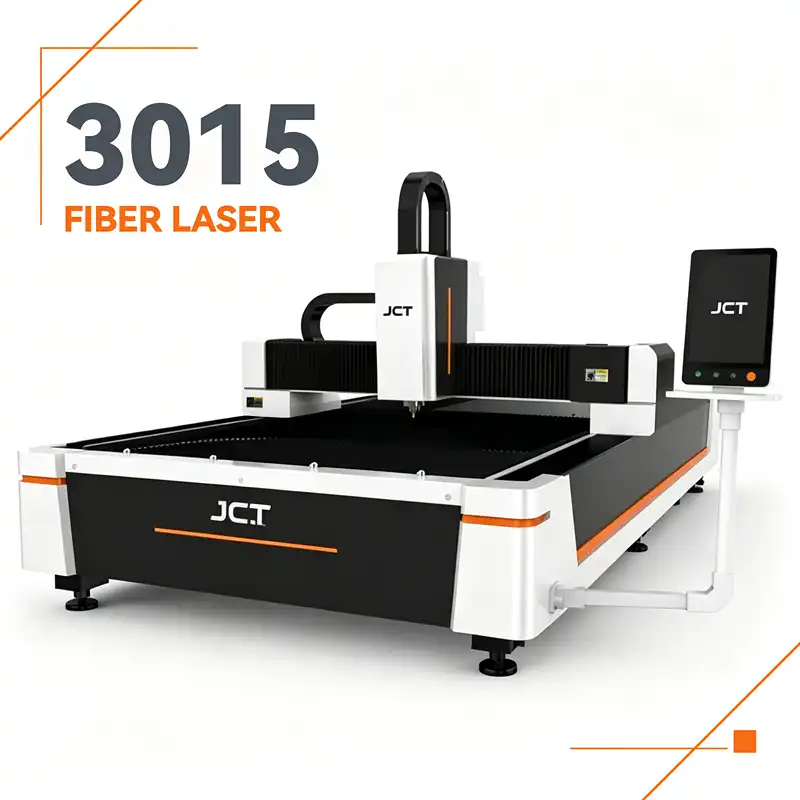
One-step weld preparation for thick structural plates requiring full-penetration AWS D1.1 welds.
Equipped with an intelligent 3D cutting head that swings up to 45 degrees. It profiles the part and cuts complex V, Y, X, and K bevels simultaneously. Eliminates the need to transport heavy plates to secondary mechanical bevelers, cutting processing time by 70%.
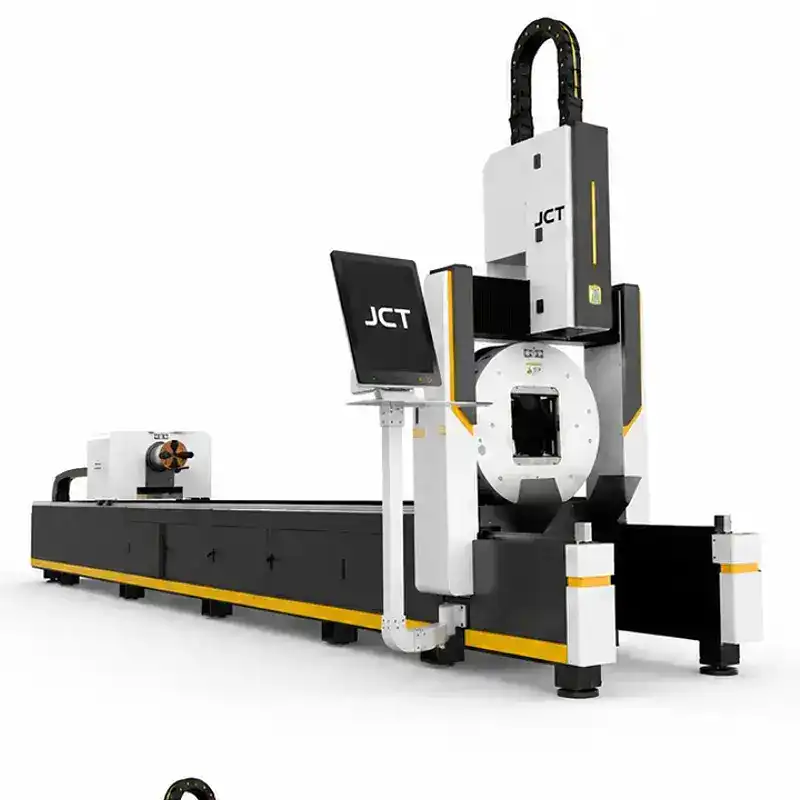
ROPS/FOPS cabins, structural H-beams, and heavy rectangular chassis frameworks.
Built with a massive chuck system capable of holding tubes up to 350mm in diameter and weighing over 1000kg. It automatically cuts complex intersections and slots on heavy profiles, ensuring zero-gap fit-ups for robotic welding cells.
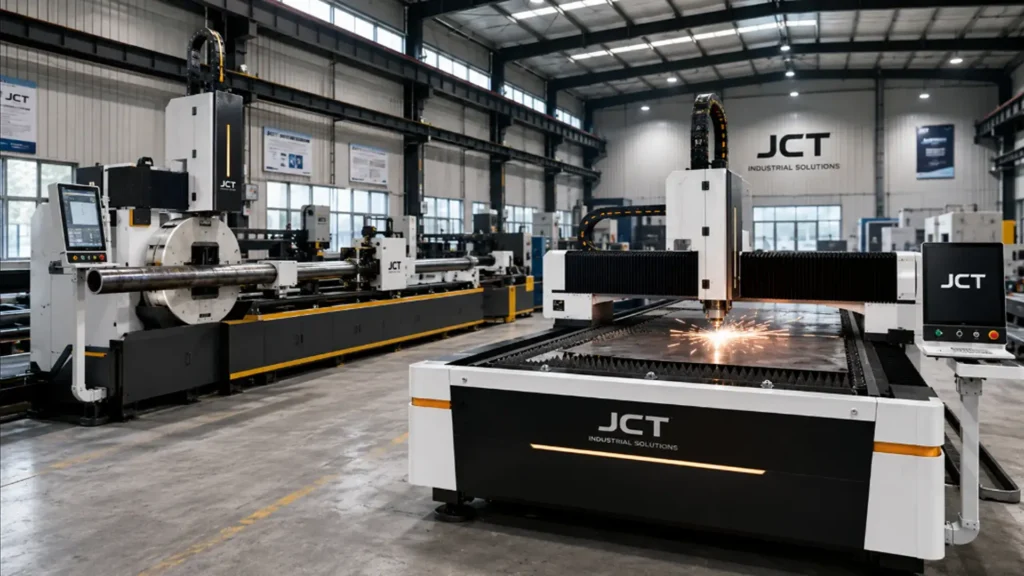
WHO WE ARE?
Manufacturingthe Future of Laser Fabrication & Quality Control.
With over 10 years of industry expertise, we have grown into a trusted source for industrial laser welding & cutting fabrication processing systems and precision environmental testing equipment.
At JCT, we not only build machines; but also build reliability.
As an original source factory, we manage the entire chain from custom CAD design and sheet metal fabrication to precision assembly, rigorous factory testing, direct export, and lifetime after-sales support.
When you partner with JCT, you work directly with the makers—no middlemen, no inflated markups, and zero empty promises.
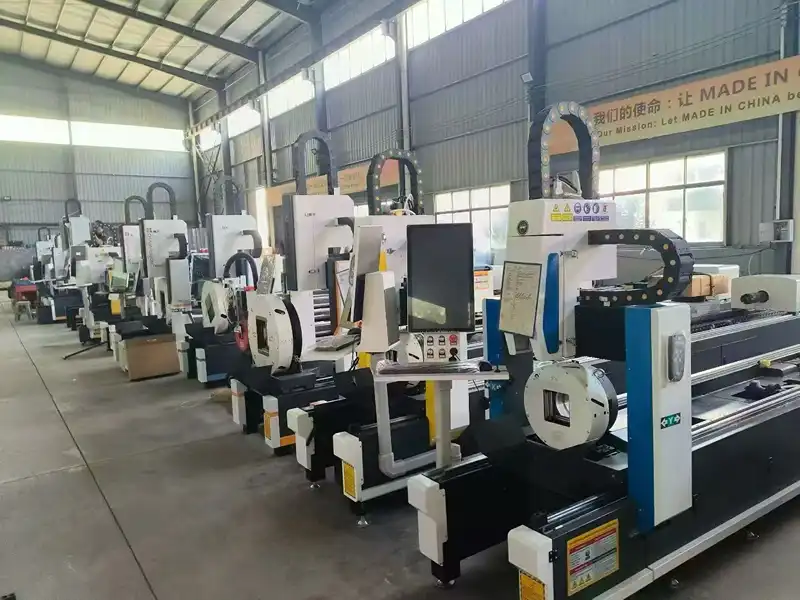
SUCCESS CASES
Trusted by Manufacturers Worldwide
From streamlining sheet metal production lines to ensuring automotive sensor components pass rigorous high- and low-temperature and humidity environmental tests, our solutions are helping customers around the world boost production efficiency and improve quality. Learn how we help our customers overcome their toughest manufacturing and testing challenges.
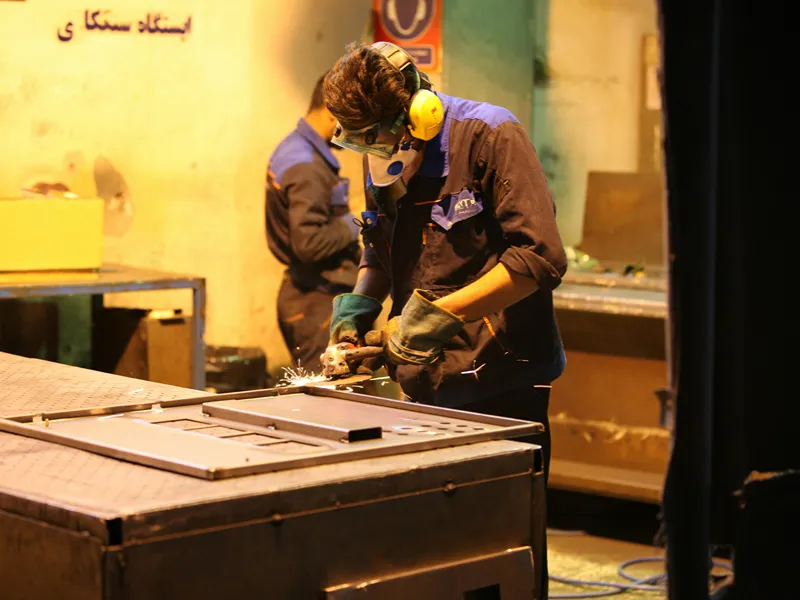
Discover how an Australian manufacturer used our laser solutions to solve the problem of recruiting skilled welders and completely eliminate the need for post-welding secondary grinding
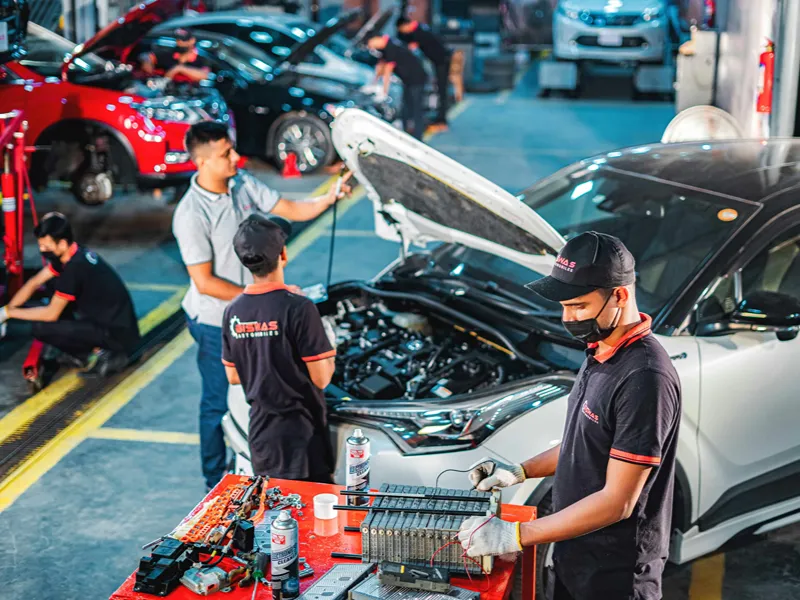
See how a Tier-2 supplier from North America used our temperature shock chamber to pass strict automotive certifications and secure a global contract
Learn how an electrical cabinet manufacturer from Dubai ,used our industrial laser welders to eliminate weld spatter and thermal distortion, then their electrical cabinet products achieved a 100% first-pass yield rate and successfully passed IP66 outdoor certification.
Learn how a Southeast Asian smart home brand used our environmental chamber to conduct accelerated aging tests, optimize PCB coatings, and significantly reduce their global return rate.
PREMIUM COMPONENTS ASSURANCE
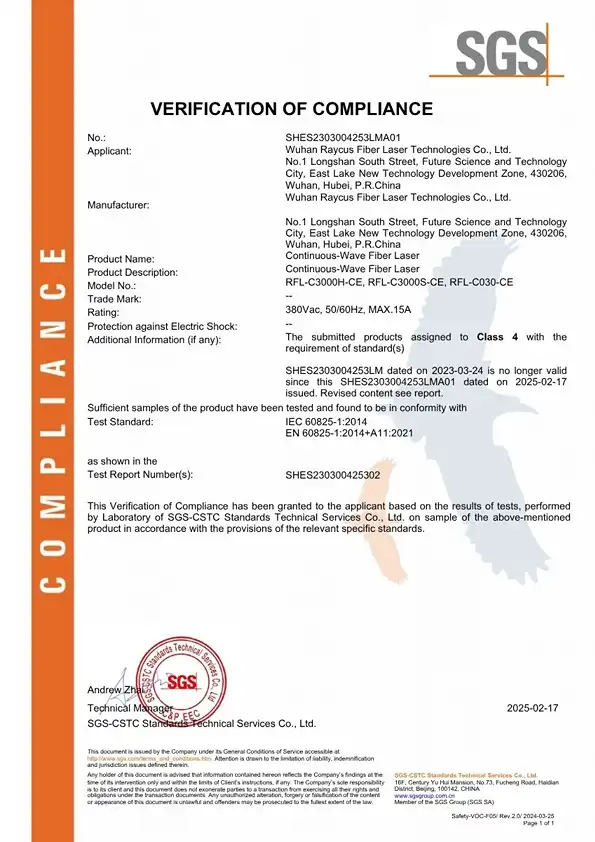
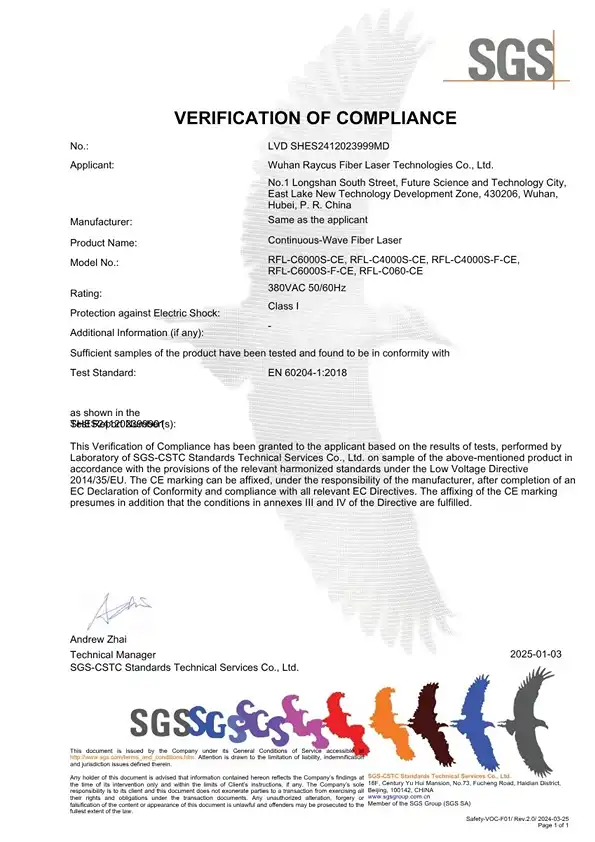
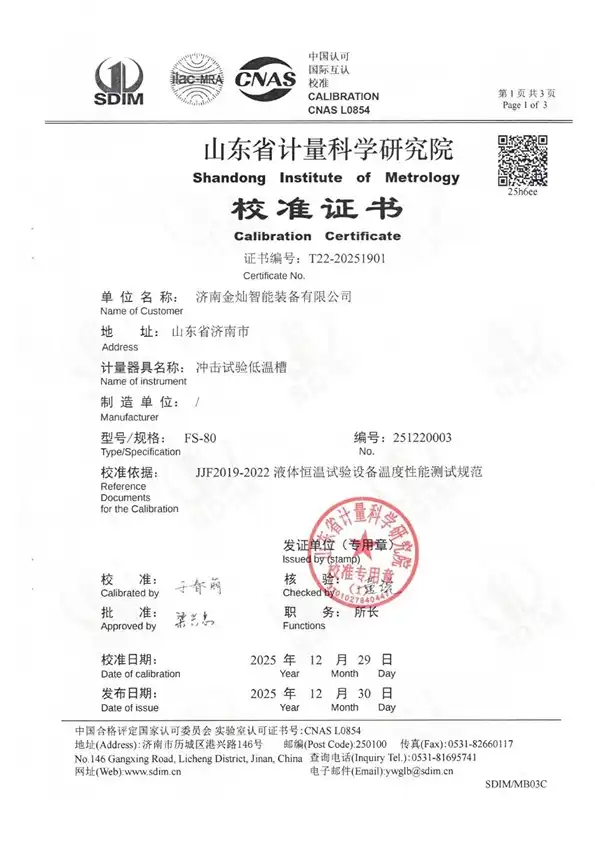
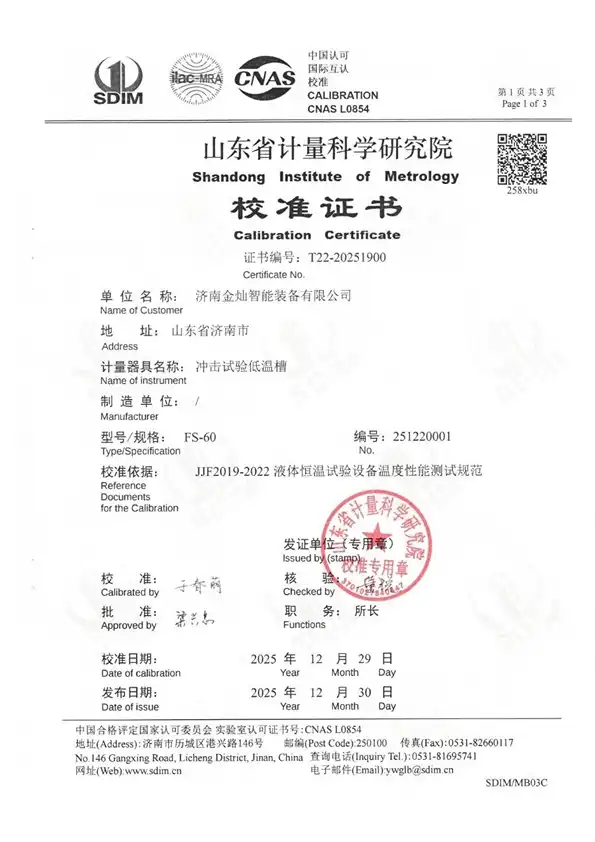
Certified to Global Leading Standards
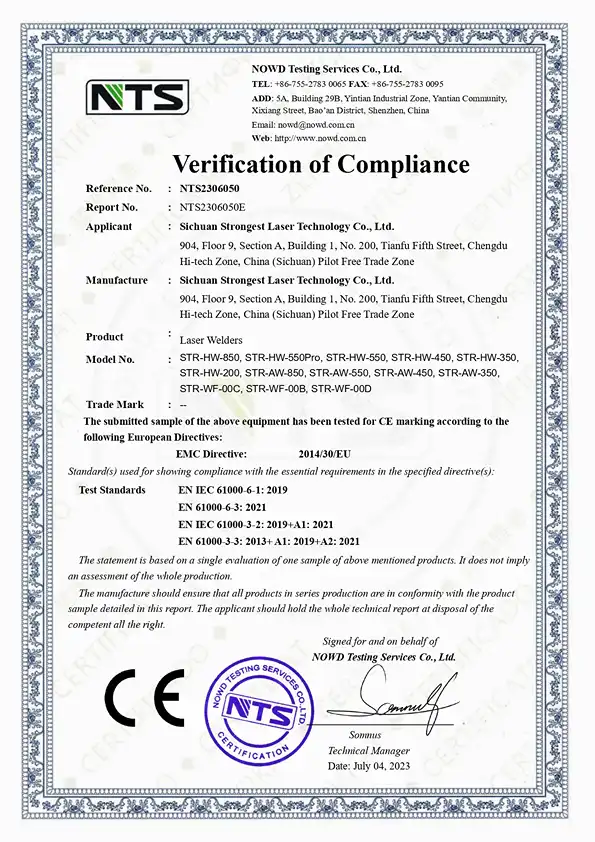
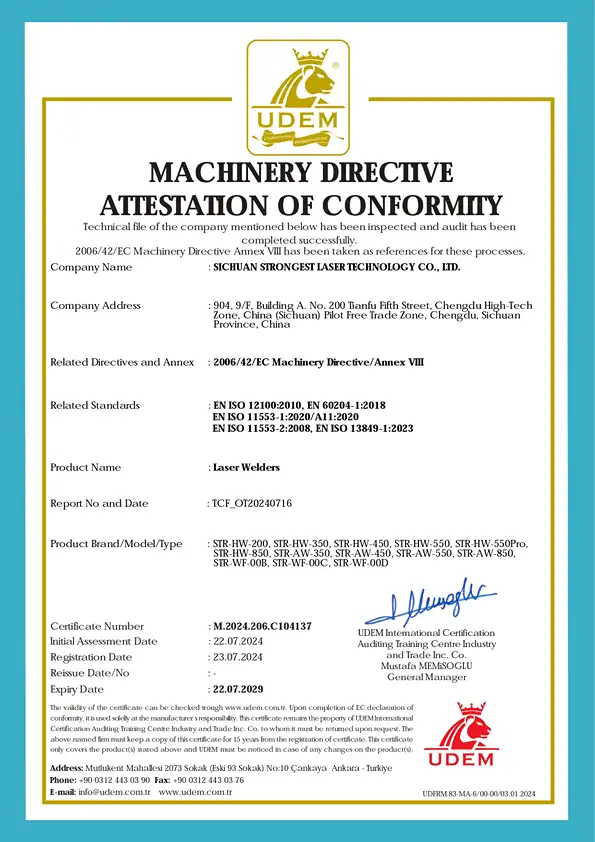
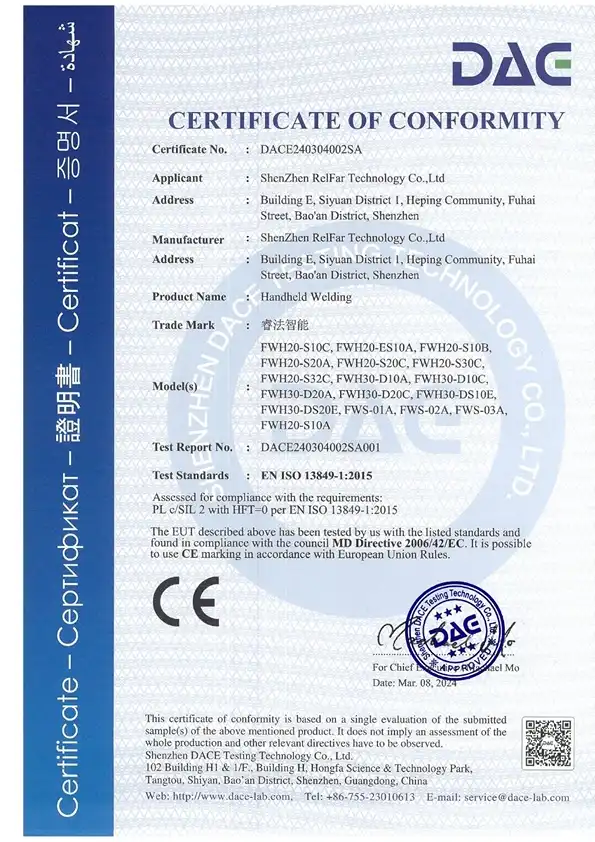
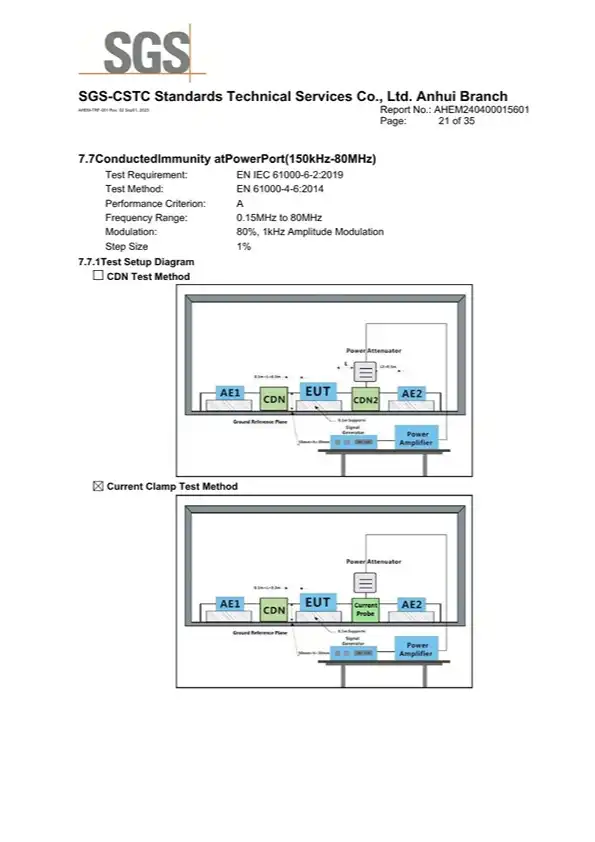
Reliability starts at the core. The key components that power our equipment—from the laser source to even the smallest electronic components—have all been certified to meet the world’s most stringent international standards.
GLOBAL PARTNERSHIPS
Trusted by Industry Leaders Worldwide
We take pride in powering the success of top-tier global manufacturers, research institutions, and industrial leaders. Our advanced laser and testing solutions are trusted worldwide to deliver uncompromising quality and peak performance.
FAQ
Q1: We currently use HD Plasma for 30mm carbon steel. Can a laser really cut this cleanly?
Yes.
With a JCT 20kW or 30kW fiber laser, you can cut 30mm carbon steel significantly faster than plasma, with a perfectly perpendicular edge (no taper) and absolutely zero bottom dross. The parts can go straight from the laser bed to the welding or painting department.
Q2: How does 5-axis bevel cutting work on thick plates?
The cutting head uses multi-axis motors to tilt up to 45 degrees while moving along the toolpath. Using our advanced nesting software, you program the specific bevel type (V, Y, K) needed for your weld prep. The machine automatically adjusts height, angle, and power to cut the part and the bevel in one continuous pass.
Q3: We use heavy H-beams and I-beams for chassis frames. Can the tube laser handle these?
Yes. Our Heavy-Duty Tube Laser is designed for structural profiles. It utilizes powerful pneumatic chucks to grip irregular shapes like H-beams and channel steel. The laser maps the profile to compensate for mill bowing, ensuring perfect cut geometry for structural joints
Q4: What assist gas is most economical for cutting 20mm - 40mm steel?
While Oxygen is traditionally used for thick carbon steel to aid combustion, ultra-high-power lasers (30kW+) have popularized High-Pressure Air cutting.Compared to liquid oxygen ,Using compressed, dried shop air massively reduces gas costs and provides exceptionally fast, clean cuts on medium-to-thick plates.
Q5: How difficult is it to program the bevel cutting machine?
It is highly automated. We utilize industry-leading 3D CAD/CAM nesting software. Your engineers just need to import the 3D model (e.g., STEP file) of the beveled part. The software automatically recognizes the bevel angles, generates the complex 5-axis toolpaths, and optimizes the plate nesting to minimize scrap.
Q6: What are the maintenance requirements for a 30kW+ fiber laser?
Fiber lasers are solid-state and highly reliable. The primary maintenance involves keeping the protective optics (cover glasses) clean from heavy cutting dust, ensuring the high-capacity water chiller is maintained, and regularly changing the air compressor filters if using air cutting. The laser source itself is virtually maintenance-free.
Q7: What is the ROI versus buying a new HD Plasma table and a mechanical beveler?
ROI for heavy machinery plants is typically 12 to 18 months. You are not just replacing a cutting machine; you are eliminating the entire secondary machining department (no more grinding dross, drilling holes, or mechanical edge milling)
Related Products
Get a Factory-Direct Custom Quote
Stop wasting machine shop hours squaring up tapered plasma cuts and grinding bevels.
Tell our application engineers about your specific plate thicknesses, material grades (e.g., Carbon Steel, Hardox), and production bottlenecks. We will recommend the exact ultra-high-power JCT laser configuration to upgrade your heavy fabrication line, complete with a factory-direct quote within 12 hours.